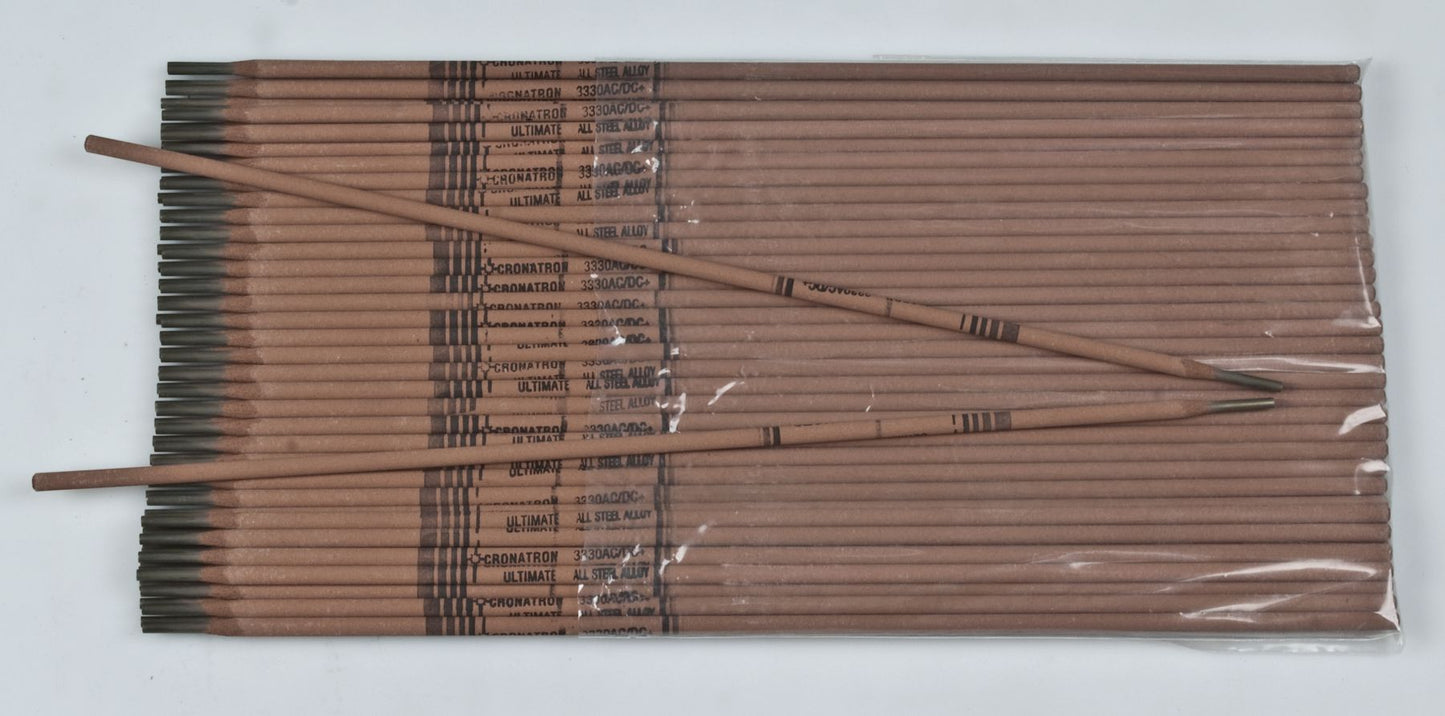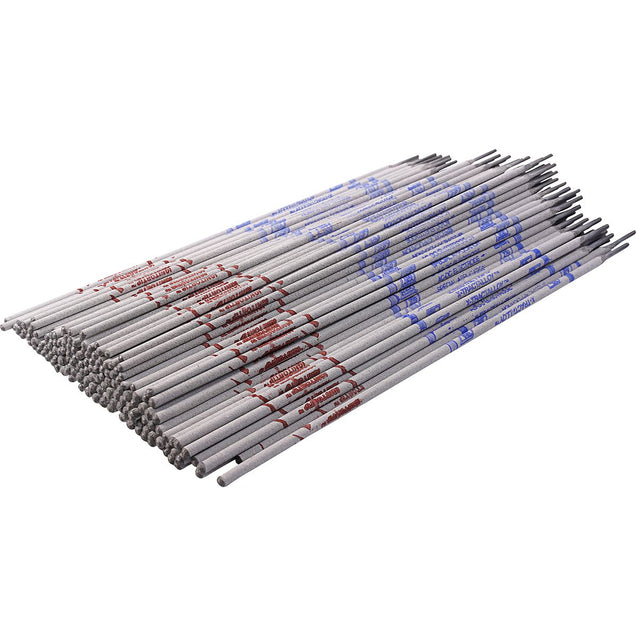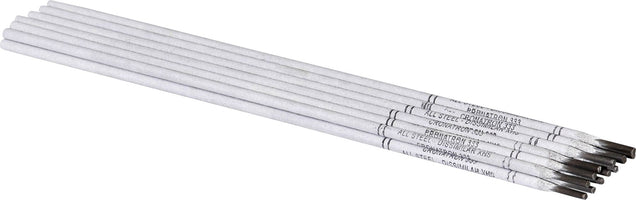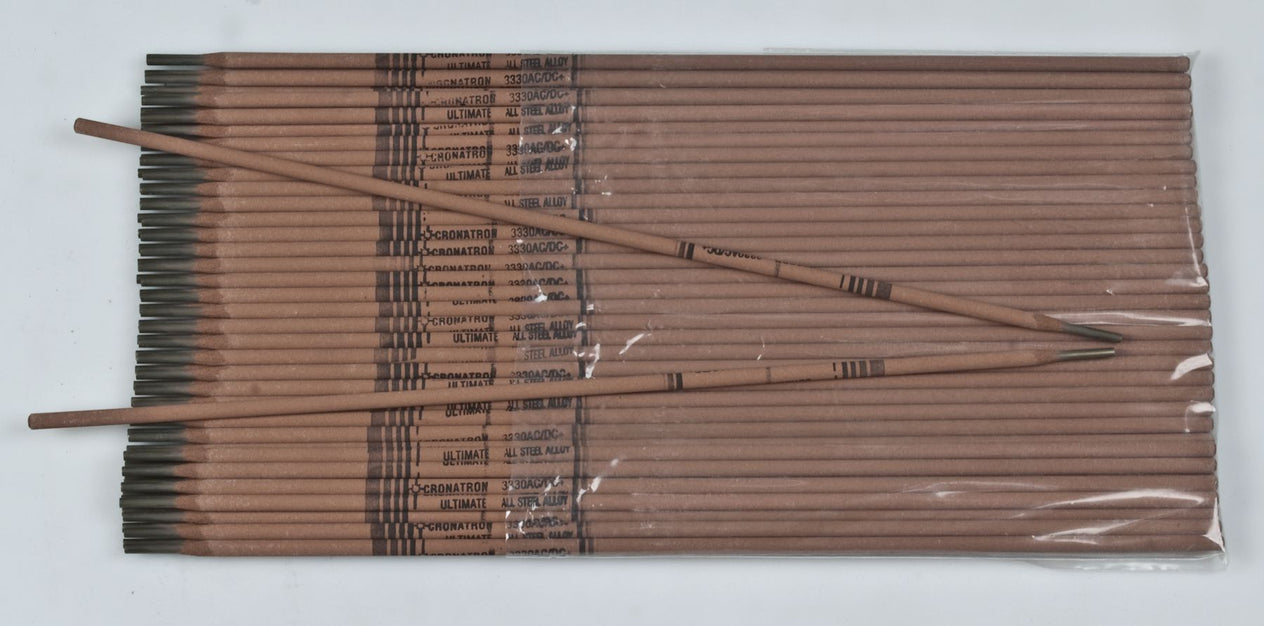
3330 Dissimilar Steel Stick Rod Electrode, Flux Coated, 75 to 100 Amps, 35% Elongation, DCRP/AC Polarity, 1/8"
(Pack of
5)
SKU:CW1873 Item#: CW1873
High-strength, dissimilar steel joining. Excels in out-of-position applications. Vertical-up and overhead.
Exceptional out-of-position welding
Tensile Strength: 127,000 PSI
Elongation: 37%
Hardness: 235 BHN
Polarity: AC or DC Reverse
Usage ProcedureUse AC or DC reverse polarity. Electrode may be used in a contact “drag” fashion or by holding a short arc. Stringer beads or a slight weave is best. Remove slag between passes. When welding alloyed or tool steel, preheat according to base metal requirements. For vertical-up welding, use a 1/8" electrode at approximately 65 to 70 amps or a 5/32" electrode at 75 to 85 amps. Use a weave “ledge” technique, pausing momentarily at end of weaves.
Frequently Bought Together
X-Tractalloy Extracting Stick Electrode 5/64
Couldn't load pickup availability
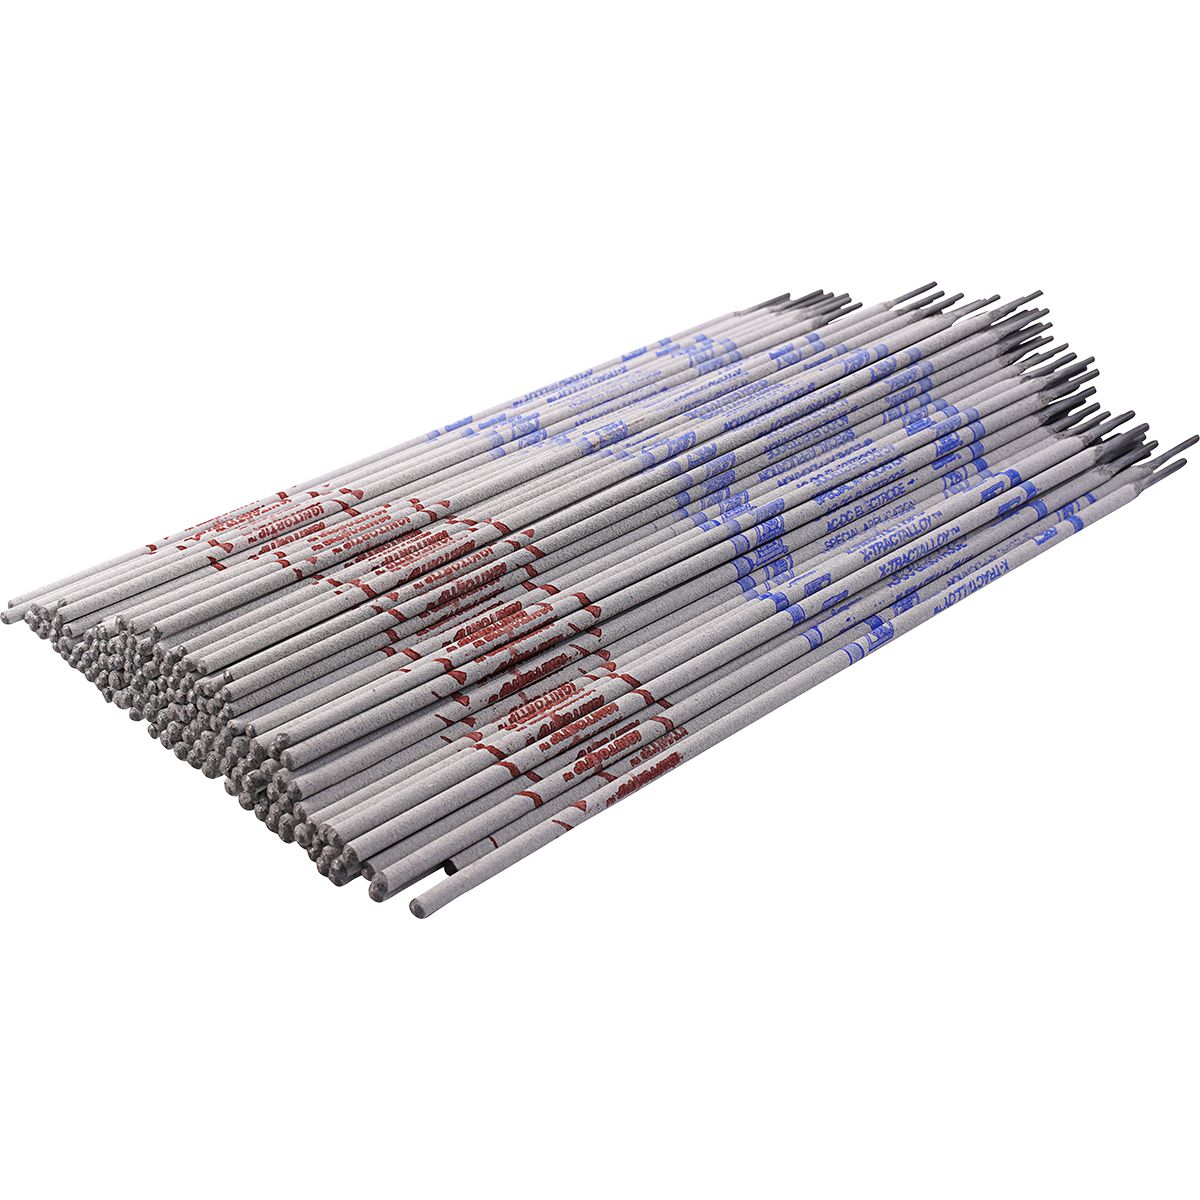
X-Tractalloy Welding Electrode Non-Conductive Flux 3/32 5/64 2LBS EA
Couldn't load pickup availability
100 Blue Lightning Tough Duplex Alloy 1/8
Couldn't load pickup availability
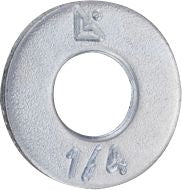
SAE Flat Washer Thru-Hardened Steel 1/4"
Couldn't load pickup availability

SAE J995C Locknut with Nylon Insert Grade 8 1/2-13
Couldn't load pickup availability
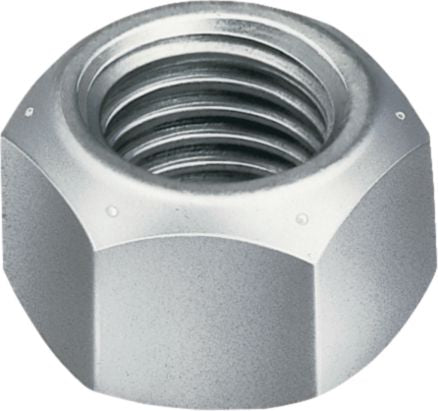
IFI 100/107 Top Locknut Grade C 5/8-11
Couldn't load pickup availability
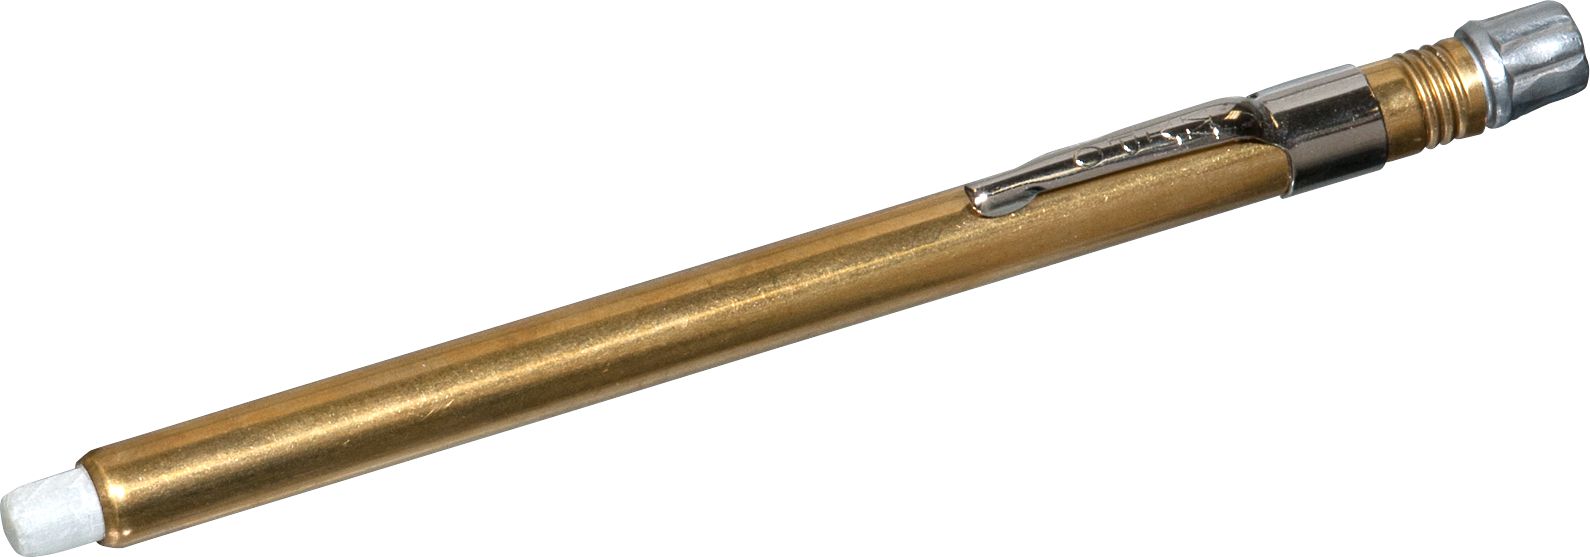
Round Soapstone Holder Heavy Duty
Couldn't load pickup availability
321 Mild and Carbon Steel MIG Welding Wire 0.035"
Couldn't load pickup availability
Oxy Acetylene Fuel and Oxygen Quick Connector
Couldn't load pickup availability
X-Tractalloy Welding Electrode Non-Conductive Flux 1/8 3/32 1LB EA
Couldn't load pickup availability
Dissimilar Steel Stick Rod Electrode Kit
Couldn't load pickup availability
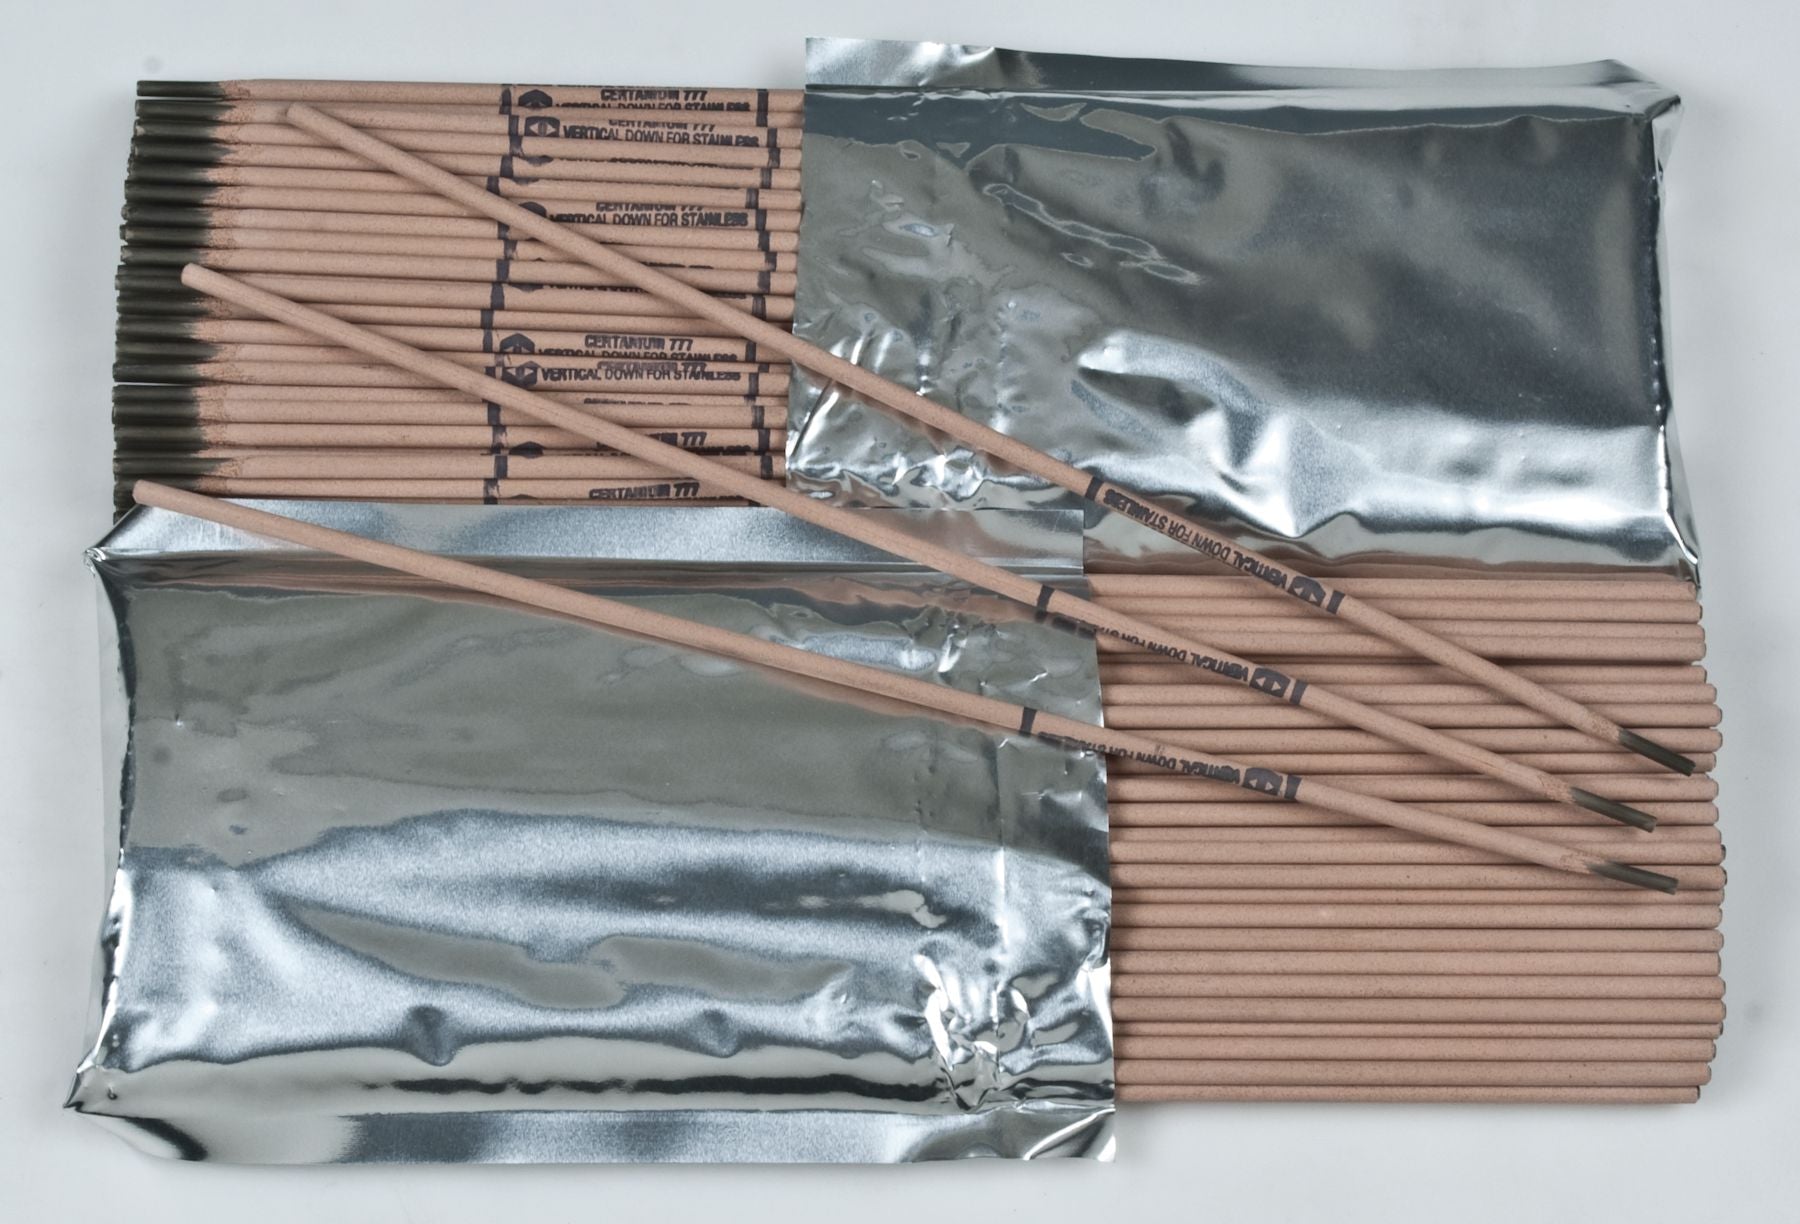
777 Stainless Steel Stick Rod Electrode 1/8"
Couldn't load pickup availability
Product Description
High-strength, dissimilar steel joining. Excels in out-of-position applications. Vertical-up and overhead.Exceptional out-of-position welding
Tensile Strength: 127,000 PSI
Elongation: 37%
Hardness: 235 BHN
Polarity: AC or DC Reverse
Usage ProcedureUse AC or DC reverse polarity. Electrode may be used in a contact “drag” fashion or by holding a short arc. Stringer beads or a slight weave is best. Remove slag between passes. When welding alloyed or tool steel, preheat according to base metal requirements. For vertical-up welding, use a 1/8" electrode at approximately 65 to 70 amps or a 5/32" electrode at 75 to 85 amps. Use a weave “ledge” technique, pausing momentarily at end of weaves.
Technical Specifications
| Item#: | CW1873 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 1/8 " |
| Tensile Strength | 125,000 PSI |
| Yield Strength | 100,000 PSI |
| Elongation | 35 % |
| Polarity | DCRP/AC |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 5.0 lb |
Product Restrictions