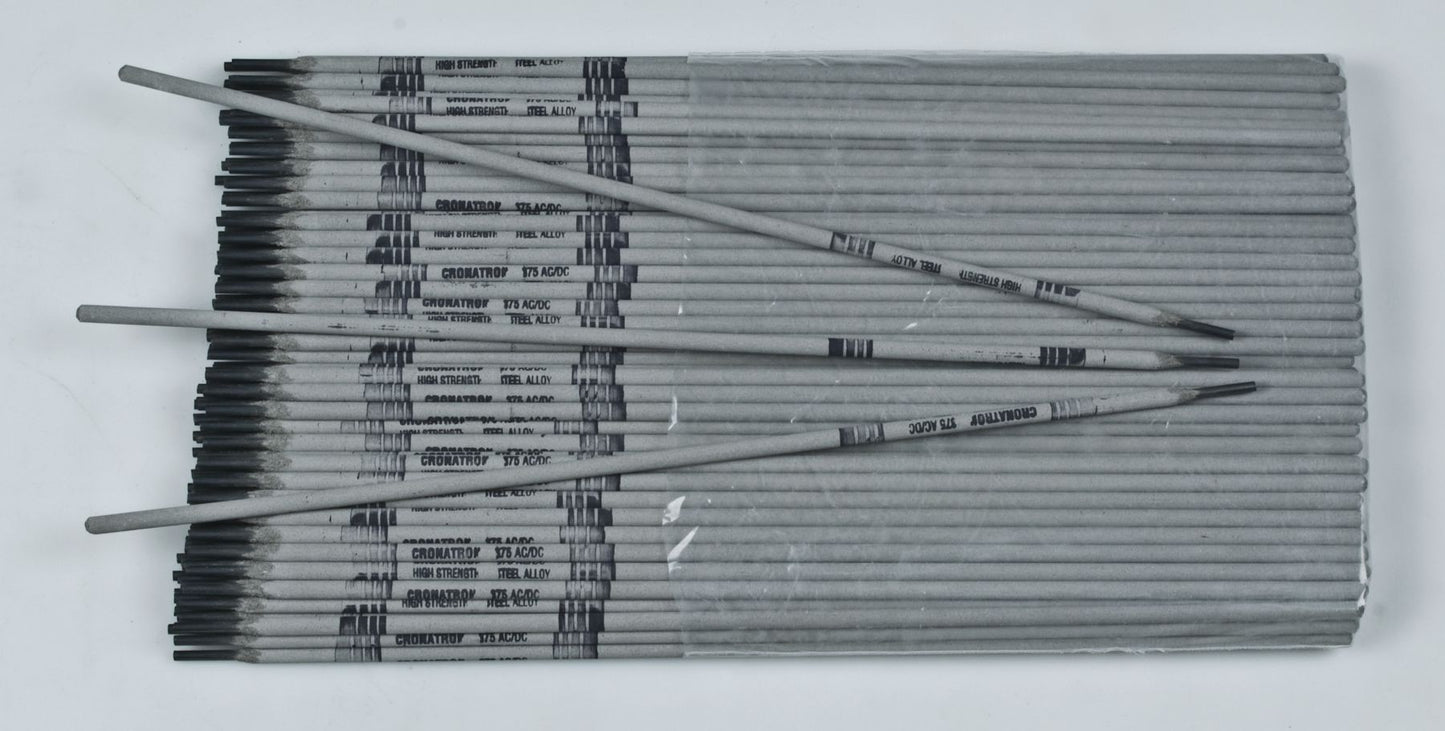
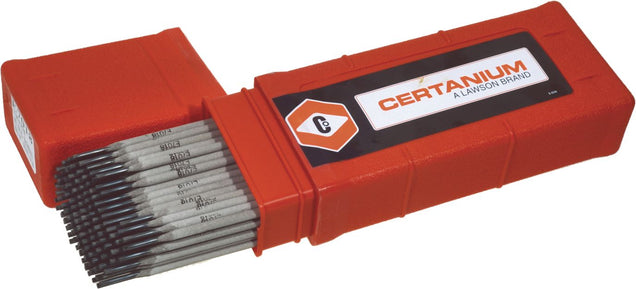
375 Mild and Carbon Steel Low Hydrogen Stick Rod Electrode, Flux Coated, 100 to 130 Amps, 18% Elongation, 1/8"
(Pack of
10)
SKU:CW1052 Item#: CW1052
Provides crack-free and porous-free welds on high-strength, carbon and cast steels.
Superior Advantages
• Saves Time
– Fast deposition rate
– Pass-over-pass with minimal slag chipping
• Easy To Use
– All-position welding
– Will not undercut or spatter
Tensile Strength: 133,400 PSI
Yield Strength: 120,500 PSI
Elongation: 18%
Hardness: Rc 20-25
Polarity: DC Reverse
Usage ProcedureUse AC or DC reverse polarity with 375. Use close arc with either stringer or weave technique. For vertical welds, use rapid weave and hesitate over each crater before extinguishing arc.
Frequently Bought Together
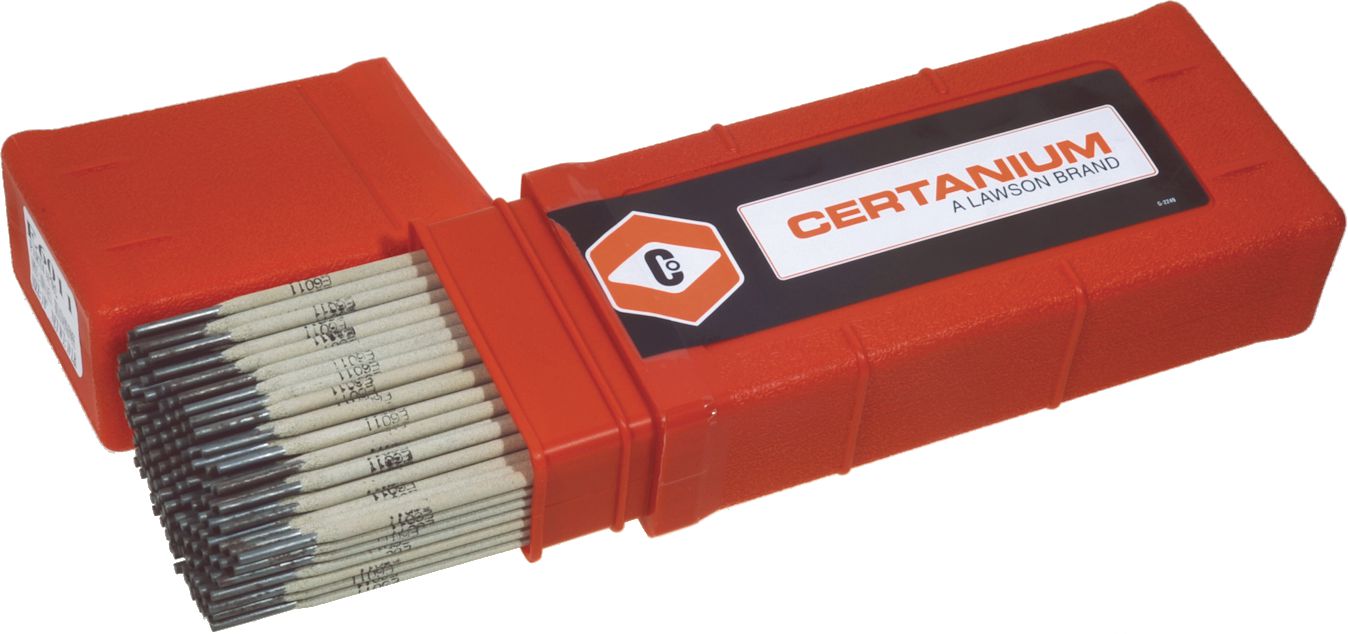
E6011 Mild/Carbon Steel Stick Electrode 5/32"
Couldn't load pickup availability
331 Mild and Carbon Steel MIG Welding Wire 0.045"
Couldn't load pickup availability
ER70S-6 Mild/Carbon Steel MIG Welding Wire 0.045"
Couldn't load pickup availability

Locknut with Nylon Insert Grade 8 5/16-18
Couldn't load pickup availability
Cross-Over Socket Extension Set, 3/8" Drive, 3 Piece
Couldn't load pickup availability
PTO Pin Lock 1/4 x 2-1/2"
Couldn't load pickup availability
321 Mild and Carbon Steel MIG Welding Wire 0.035"
Couldn't load pickup availability
Oxy Acetylene Fuel and Oxygen Quick Connector
Couldn't load pickup availability
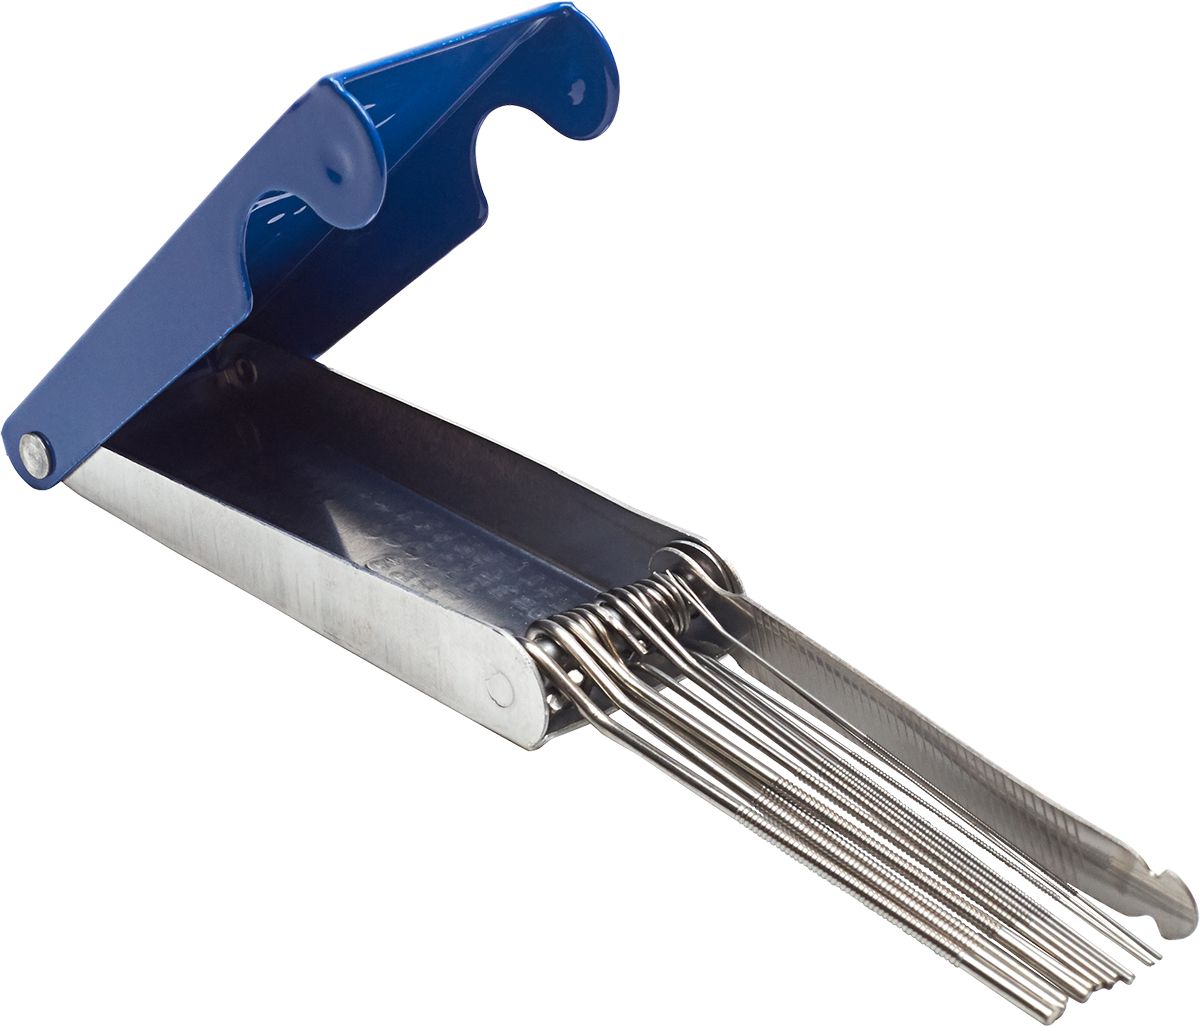
Oxy Acetylene Fuel Gas Tip Cleaner
Couldn't load pickup availability
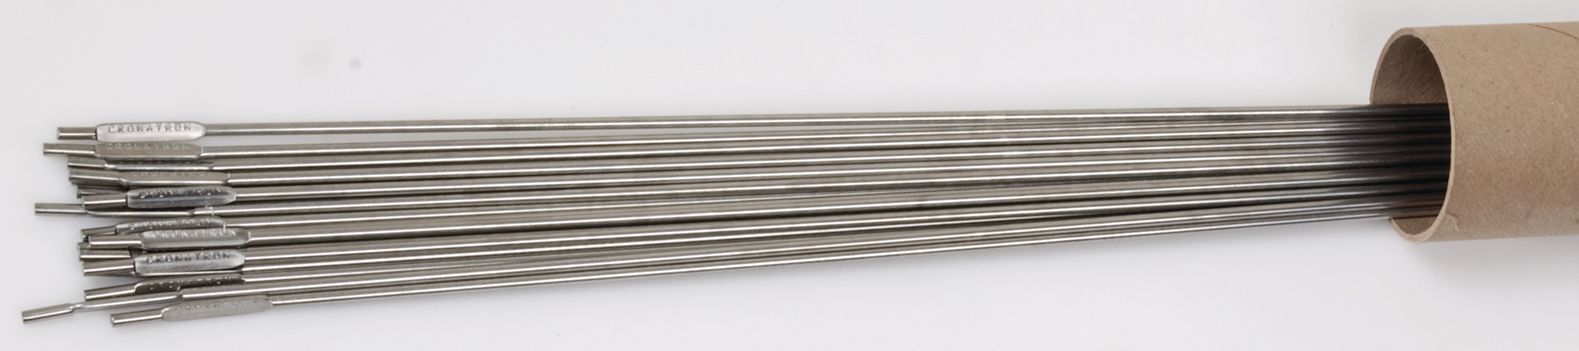
333 Dissimilar Steel TIG Wire 1/8"
Couldn't load pickup availability
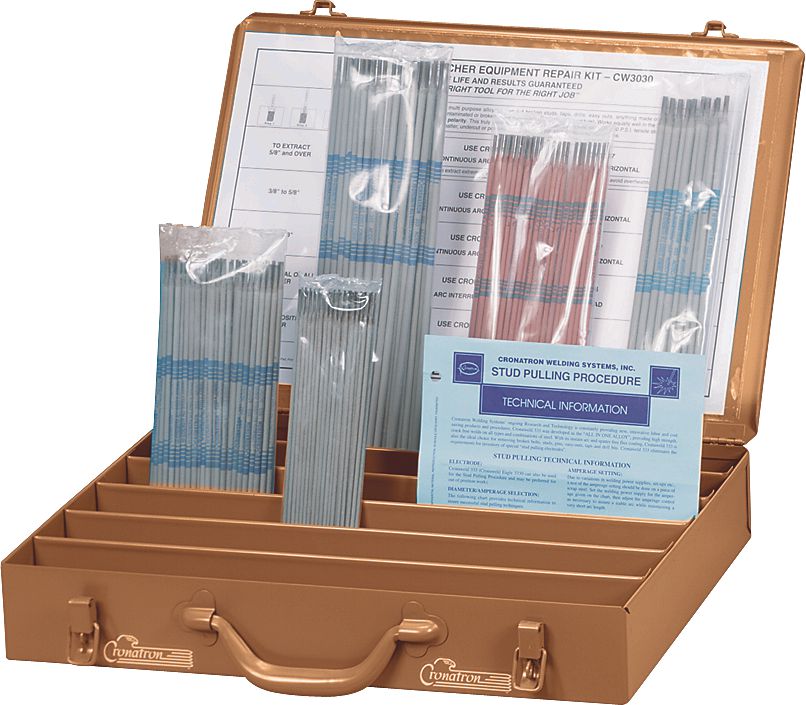
Dissimilar Steel Stick Rod Electrode Kit
Couldn't load pickup availability
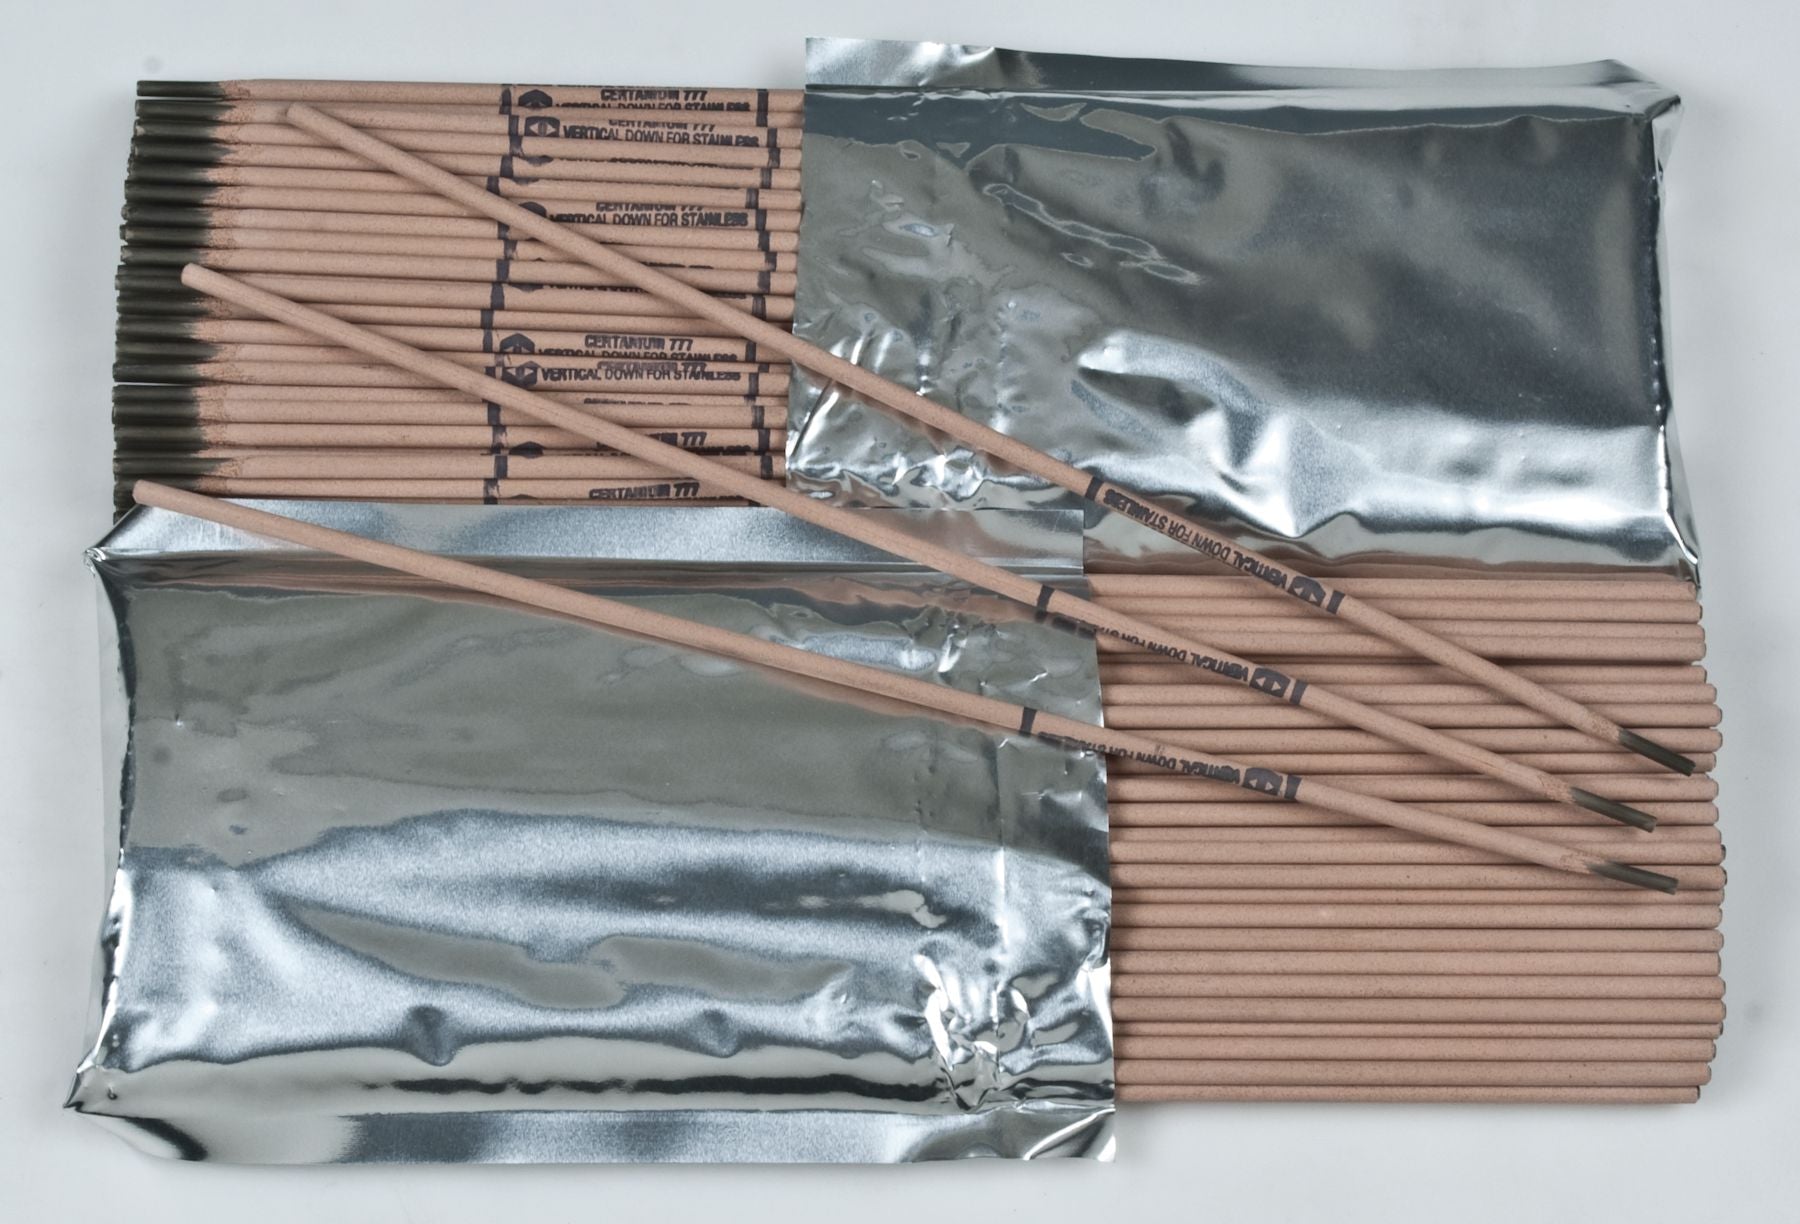
777 Stainless Steel Stick Rod Electrode 1/8"
Couldn't load pickup availability
Product Description
Provides crack-free and porous-free welds on high-strength, carbon and cast steels.Superior Advantages
• Saves Time
– Fast deposition rate
– Pass-over-pass with minimal slag chipping
• Easy To Use
– All-position welding
– Will not undercut or spatter
Tensile Strength: 133,400 PSI
Yield Strength: 120,500 PSI
Elongation: 18%
Hardness: Rc 20-25
Polarity: DC Reverse
Usage ProcedureUse AC or DC reverse polarity with 375. Use close arc with either stringer or weave technique. For vertical welds, use rapid weave and hesitate over each crater before extinguishing arc.
Technical Specifications
| Item#: | CW1052 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 1/8 " |
| Tensile Strength | 133,400 PSI |
| Yield Strength | 120,500 PSI |
| Elongation | 18 % |
| Base Metal | Mild & Carbon Steel |
| Hardness | 20-25 HRC |
| Polarity | DCRP |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 10.46 lb |
Product Restrictions