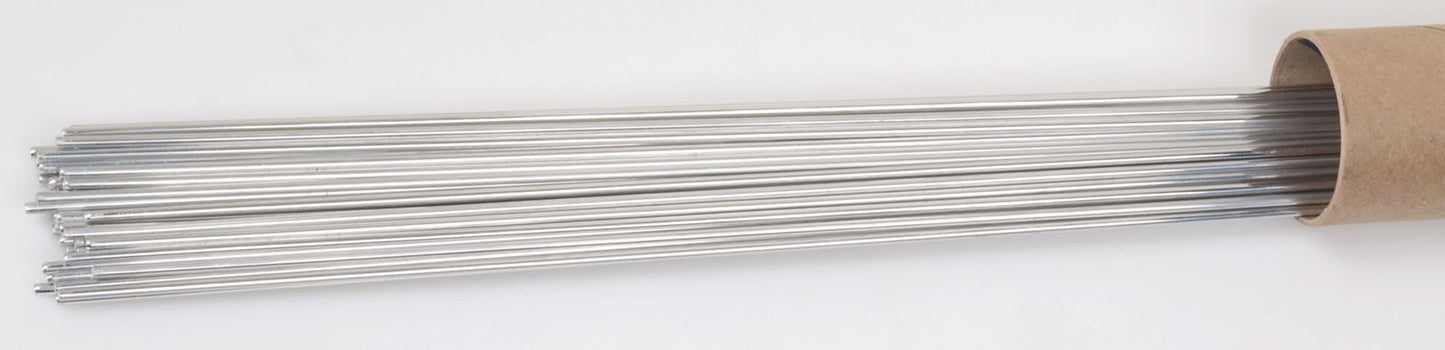
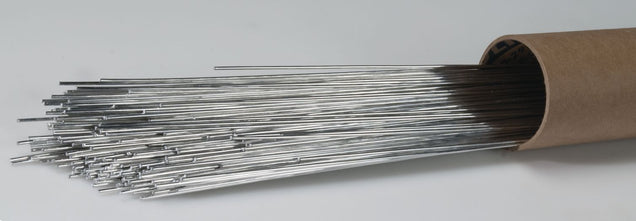
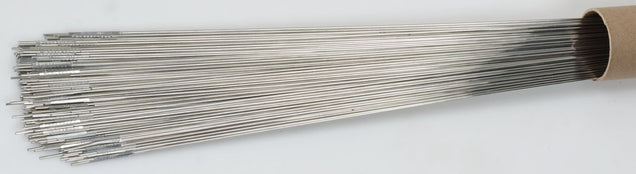
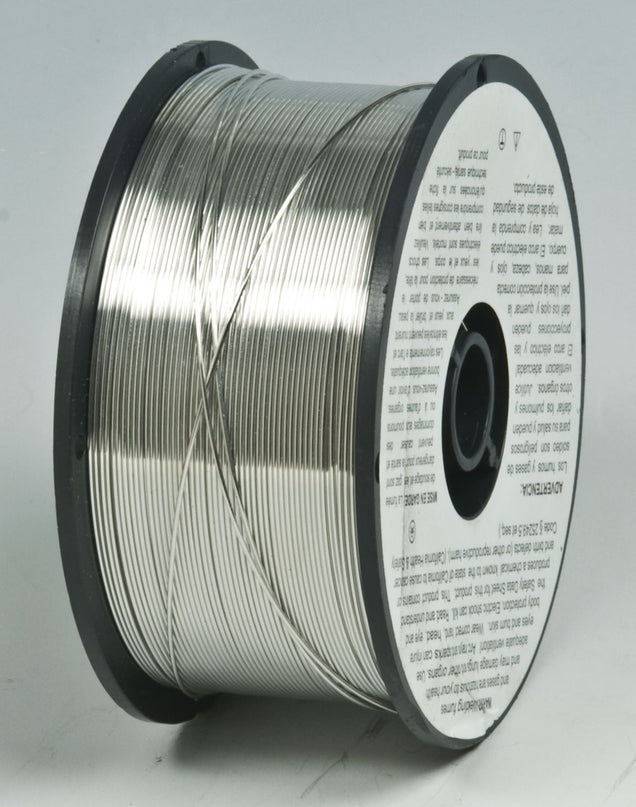
510 Aluminum TIG Wire, Solid, 100% Ar Shielding Gas, AC High Frequency Polarity, 36" Length, Quiet Arc, 1/8"
(Pack of
2)
SKU:CW1014 Item#: CW1014
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.
Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: AC/High Frequency
Gas: Argon/Helium
Usage ProcedureBevel heavy sections to allow 100% weld metal penetration. Sprinkle F56 flux into the joint area. Broadly heat area to be brazed with a large, soft and slightly carburizing flame to about 1,100°F (593°C). Heat the base metal until flux flows freely. The alloy will then begin to wet the base metal. Deposit the 510T to fill the joint. Flux residue may be removed with warm water and a brush.
Couldn't load pickup availability
Catalog page#: 13-16
Frequently Bought Together
ER5356 Aluminum TIG Wire 1/16"
Couldn't load pickup availability
556 Aluminum TIG Wire 3/32"
Couldn't load pickup availability
ER4043 Aluminum TIG Wire 3/32"
Couldn't load pickup availability

180-degree Wide Beam Head Light with Side Light
Couldn't load pickup availability
USS Flat Washer Thru-Hardened Steel 3/8"
Couldn't load pickup availability
Nylon Cable Tie 4" Black
Couldn't load pickup availability
Oxy Acetylene Fuel Gas Single Replacement Flint
Couldn't load pickup availability
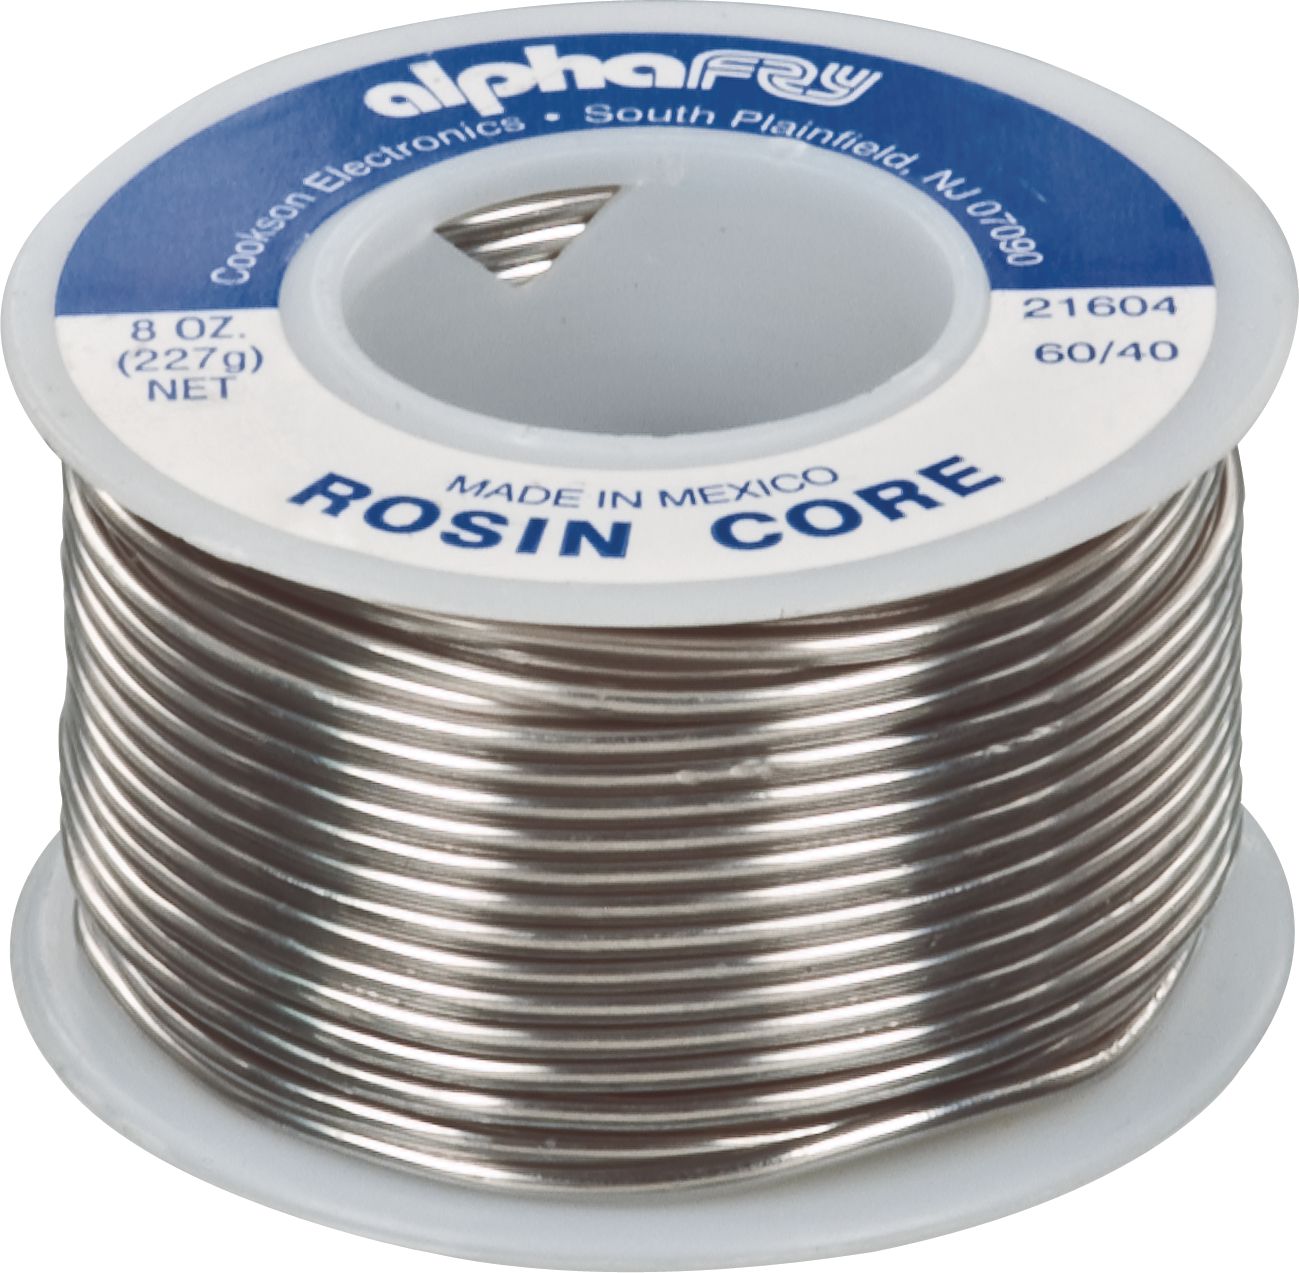
Rosin Core Solder 1/16"
Couldn't load pickup availability
Oxygen Safety Cap Heavy Duty
Couldn't load pickup availability
X-Tractalloy Extracting Welding Electrode Non-Conductive Flux 3/32
Couldn't load pickup availability
321 Mild and Carbon Steel MIG Welding Wire 0.035"
Couldn't load pickup availability
ER70S-6 Mild/Carbon Steel MIG Welding Wire 0.03"
Couldn't load pickup availability
Product Description
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: AC/High Frequency
Gas: Argon/Helium
Usage ProcedureBevel heavy sections to allow 100% weld metal penetration. Sprinkle F56 flux into the joint area. Broadly heat area to be brazed with a large, soft and slightly carburizing flame to about 1,100°F (593°C). Heat the base metal until flux flows freely. The alloy will then begin to wet the base metal. Deposit the 510T to fill the joint. Flux residue may be removed with warm water and a brush.
Technical Specifications
| Item#: | CW1014 |
|---|---|
| Welding Process | TIG |
| Type | Solid |
| Diameter | 1/8 " |
| Length | 36 " |
| Tensile Strength | 35,000 PSI |
| Base Metal | Aluminum |
| Shielding Gas | 100% Ar |
| Polarity | AC High Freq |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 2.0 lb |