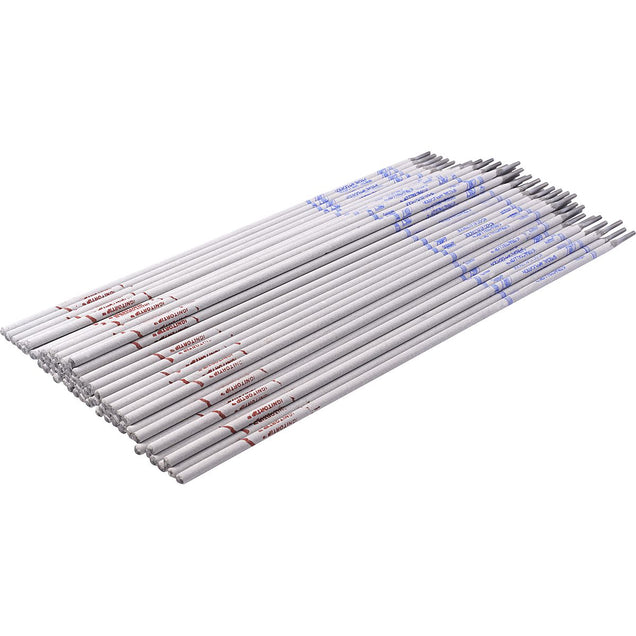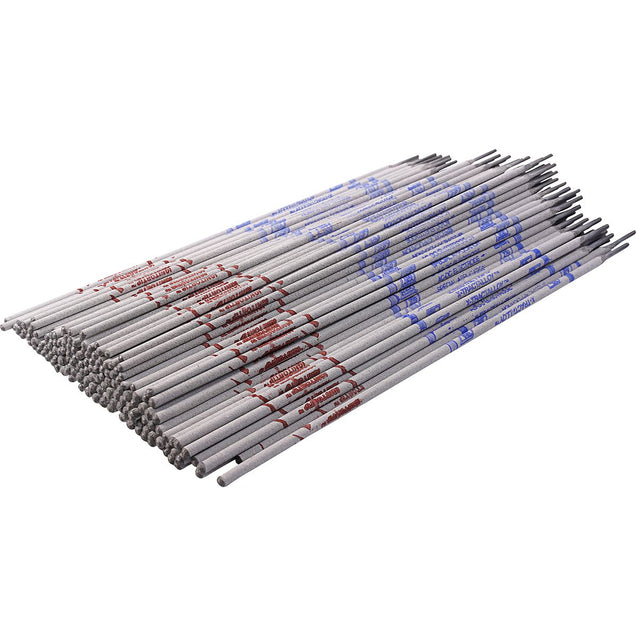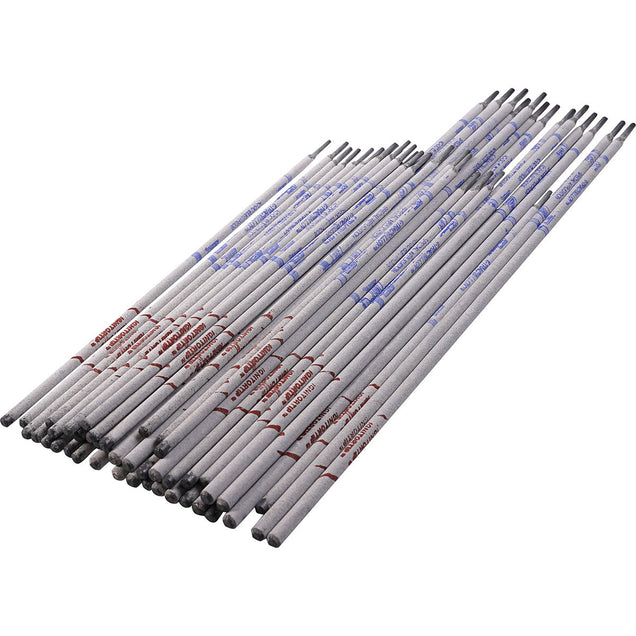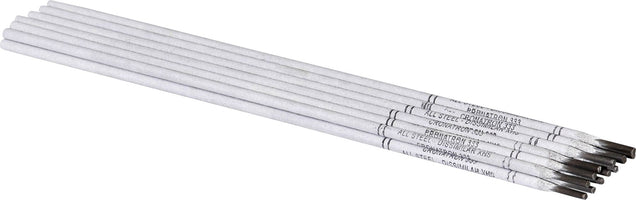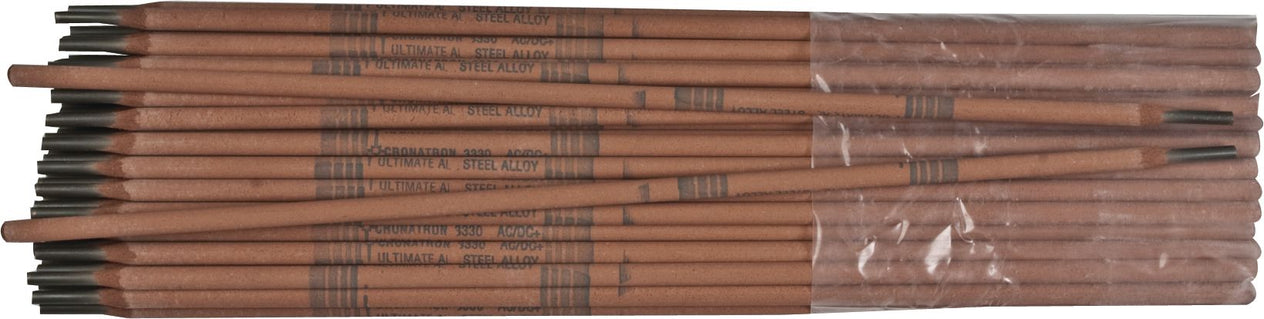
3330 Dissimilar Steel Stick Rod Electrode, Flux Coated, 100 to 145 Amps, 35% Elongation, DCRP/AC Polarity, 5/32"
(Pack of
5)
SKU:CW1872 Item#: CW1872
High-strength, dissimilar steel joining. Excels in out-of-position applications. Vertical-up and overhead.
Exceptional out-of-position welding
Tensile Strength: 127,000 PSI
Elongation: 37%
Hardness: 235 BHN
Polarity: AC or DC Reverse
Usage ProcedureUse AC or DC reverse polarity. Electrode may be used in a contact “drag” fashion or by holding a short arc. Stringer beads or a slight weave is best. Remove slag between passes. When welding alloyed or tool steel, preheat according to base metal requirements. For vertical-up welding, use a 1/8" electrode at approximately 65 to 70 amps or a 5/32" electrode at 75 to 85 amps. Use a weave “ledge” technique, pausing momentarily at end of weaves.
Frequently Bought Together

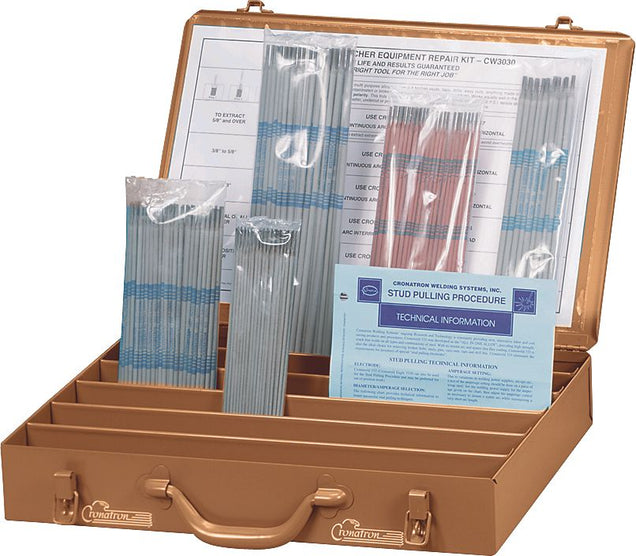
Dissimilar Steel Stick Rod Electrode Kit
Couldn't load pickup availability

X-Tractalloy Extracting Welding Electrode Non-Conductive Flux 1/8
Couldn't load pickup availability

333 Dissimilar Steel MIG Welding Wire 0.035"
Couldn't load pickup availability

Self Igniting Butane Torch
Couldn't load pickup availability

Universal Socket Set, Deep, 1/2" Drive, 24pc
Couldn't load pickup availability

Socket Set, Deep Metric, 1/2" Drive, 24pc
Couldn't load pickup availability
Self-Drilling Screw Hex Head 1/4-14 x 1"
Couldn't load pickup availability
SAE Flat Washer Thru-Hardened Steel 5/16"
Couldn't load pickup availability
USS Flat Washer Thru-Hardened Steel 5/16"
Couldn't load pickup availability
345 Tool Steel TIG Wire 1/16"
Couldn't load pickup availability
Oxy-Therm Cutting Rod 1/4 x 24"
Couldn't load pickup availability
22-50 MIG Welding Nozzle 1/2"
Couldn't load pickup availability
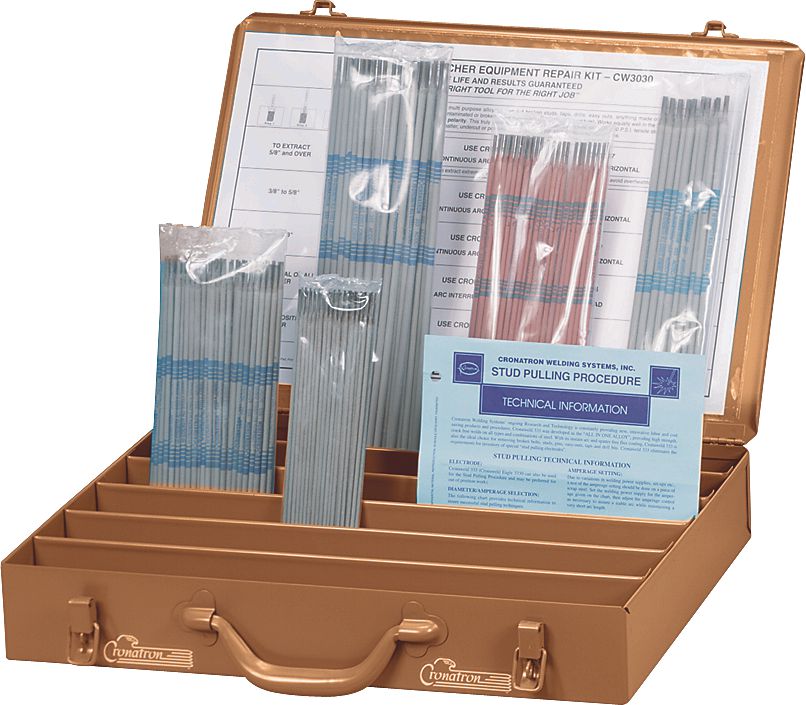
Dissimilar Steel Stick Rod Electrode Kit
Couldn't load pickup availability
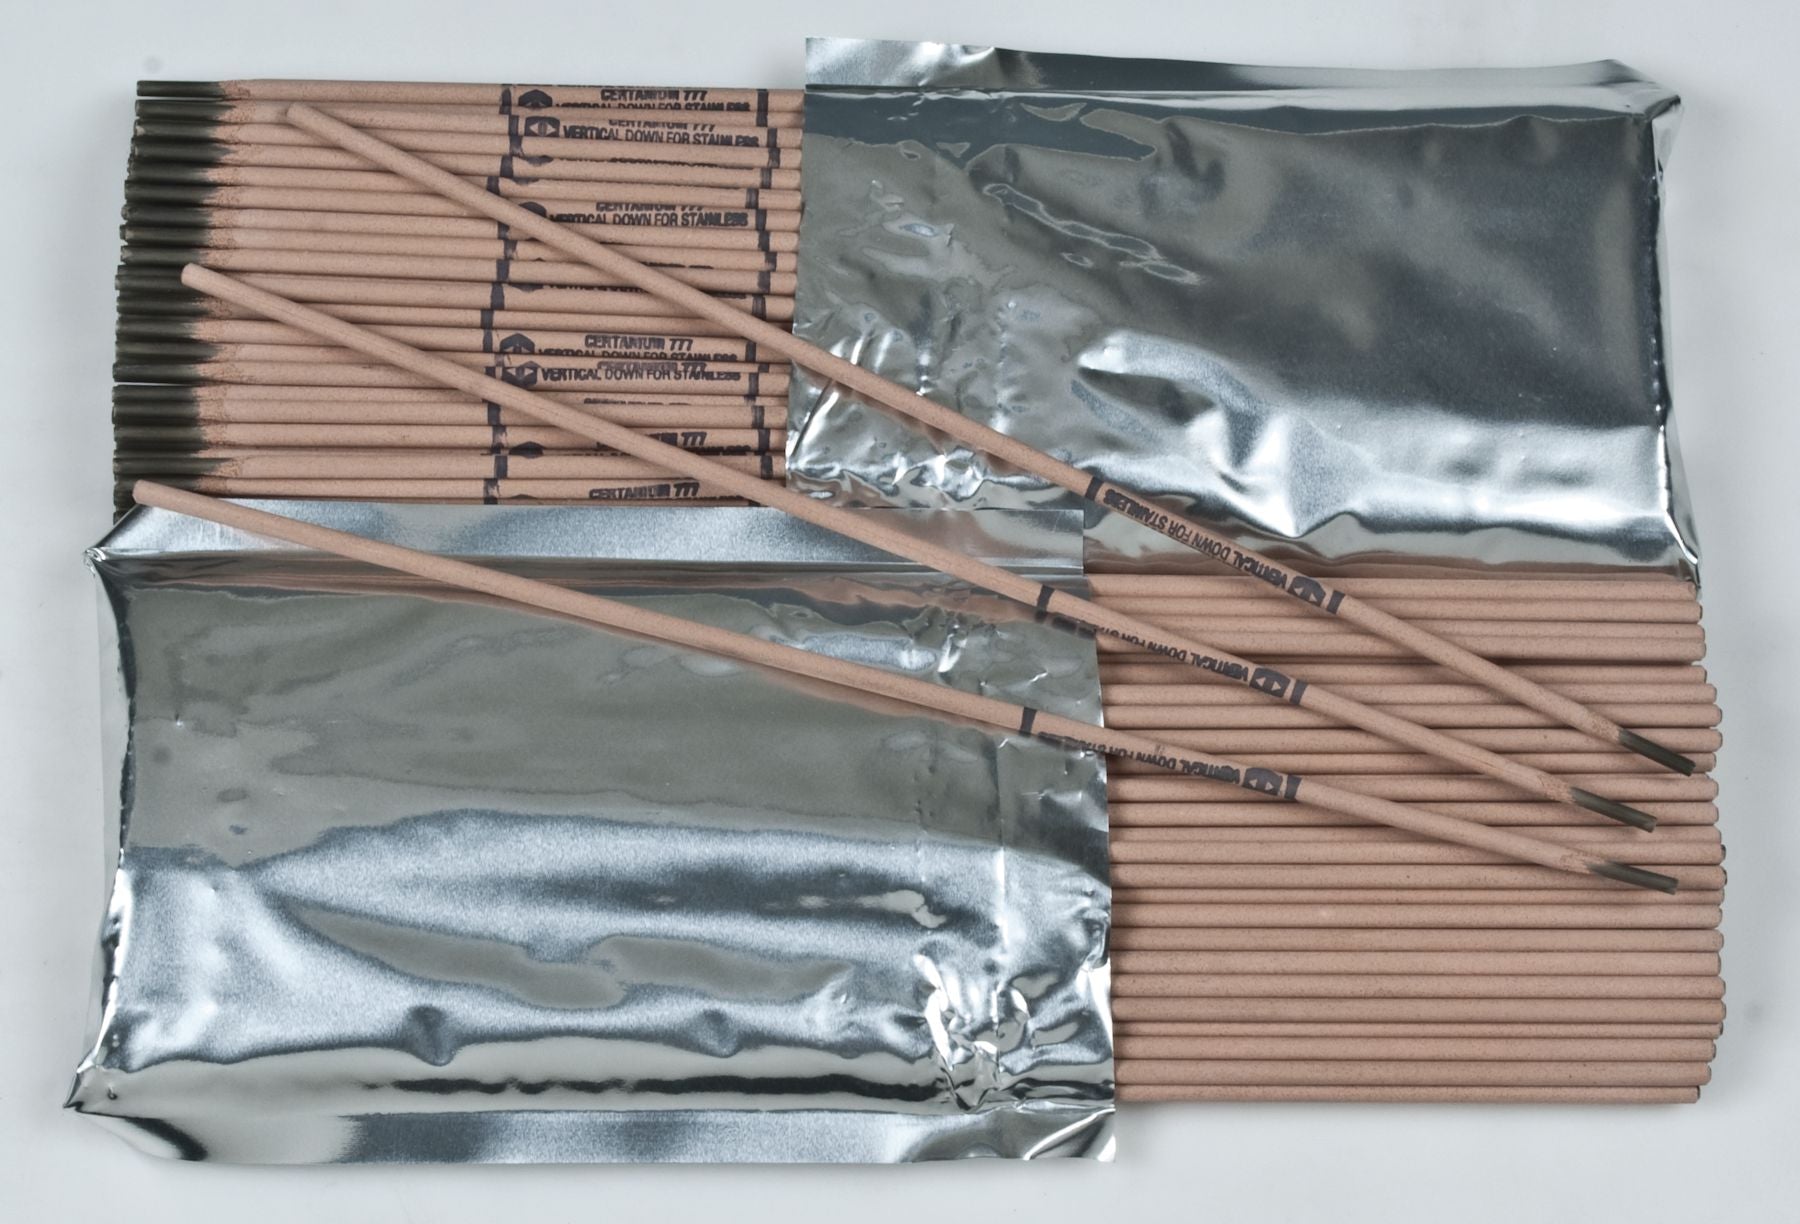
777 Stainless Steel Stick Rod Electrode 1/8"
Couldn't load pickup availability

331 Mild and Carbon Steel MIG Welding Wire 0.03"
Couldn't load pickup availability
Product Description
High-strength, dissimilar steel joining. Excels in out-of-position applications. Vertical-up and overhead.Exceptional out-of-position welding
Tensile Strength: 127,000 PSI
Elongation: 37%
Hardness: 235 BHN
Polarity: AC or DC Reverse
Usage ProcedureUse AC or DC reverse polarity. Electrode may be used in a contact “drag” fashion or by holding a short arc. Stringer beads or a slight weave is best. Remove slag between passes. When welding alloyed or tool steel, preheat according to base metal requirements. For vertical-up welding, use a 1/8" electrode at approximately 65 to 70 amps or a 5/32" electrode at 75 to 85 amps. Use a weave “ledge” technique, pausing momentarily at end of weaves.
Technical Specifications
| Item#: | CW1872 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 5/32 " |
| Tensile Strength | 125,000 PSI |
| Yield Strength | 100,000 PSI |
| Elongation | 35 % |
| Polarity | DCRP/AC |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 5.0 lb |
Product Restrictions