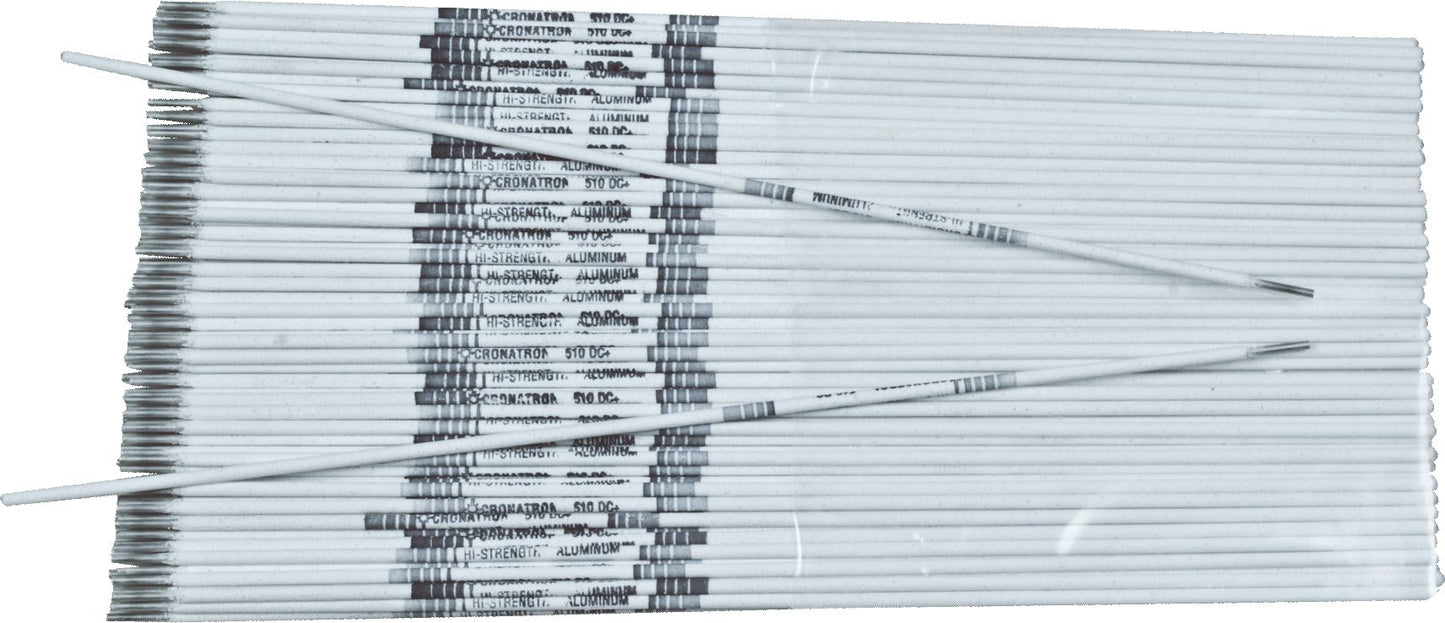
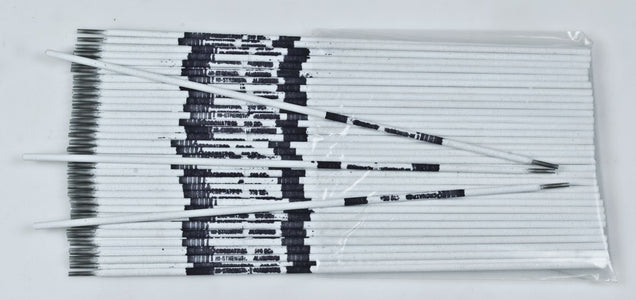
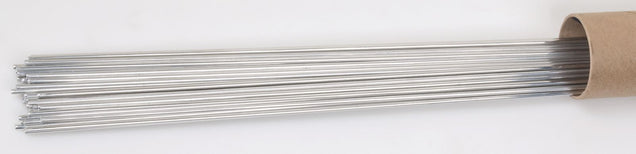
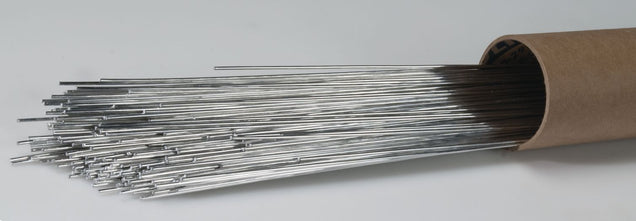
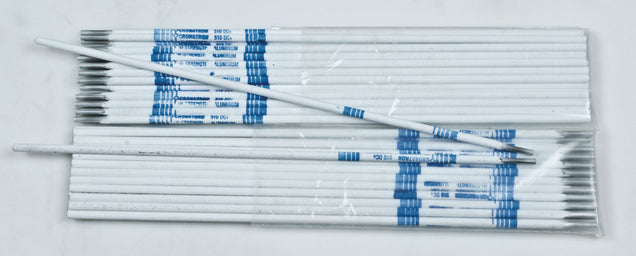
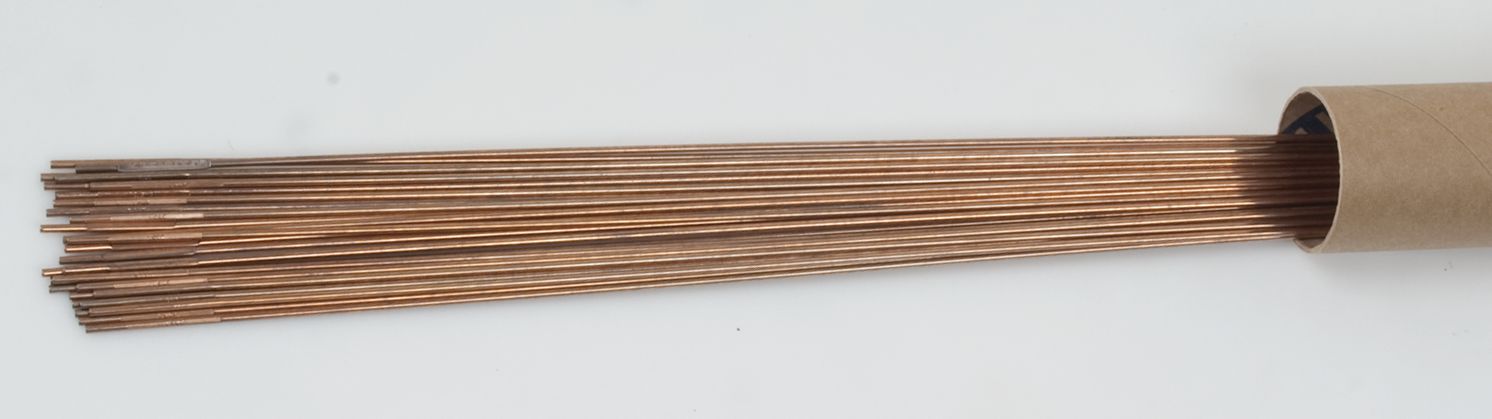
510 Aluminum Stick Rod Electrode, Flux Coated, 55 to 80 Amps, DCRP Polarity, Good Corrosion Resistance, Stable, Quiet Arc, 3/32"
(Pack of
2)
SKU:CW1826 Item#: CW1826
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.
Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: DC Reverse
Usage ProcedureMaintain the shortest arc possible, using DC reverse polarity only. On large heavy sections, preheating to 400°F (204°C) will produce faster, flatter deposit with no splatter. Electrode should be held almost perpendicular and use a rapid stringer or weaving technique with a backwhip at the crater. Bevel pieces 75° on sections 1/8" (3.2mm) or thicker.
Couldn't load pickup availability
Catalog page#: 13-16
Frequently Bought Together
ER4043 Aluminum MIG Welding Wire 0.045"
Couldn't load pickup availability
ER5356 Aluminum TIG Wire 1/8"
Couldn't load pickup availability
510 Aluminum MIG Welding Wire 0.035"
Couldn't load pickup availability

SAE J995C Locknut with Nylon Insert Grade 8 1/4-20
Couldn't load pickup availability
SAE J995C Locknut with Nylon Insert Grade 8 3/8-16
Couldn't load pickup availability
SAE Flat Washer Thru-Hardened Steel 3/8"
Couldn't load pickup availability
Rosin Core Solder 1/16"
Couldn't load pickup availability
Round Soapstone 1/4 x 5"
Couldn't load pickup availability
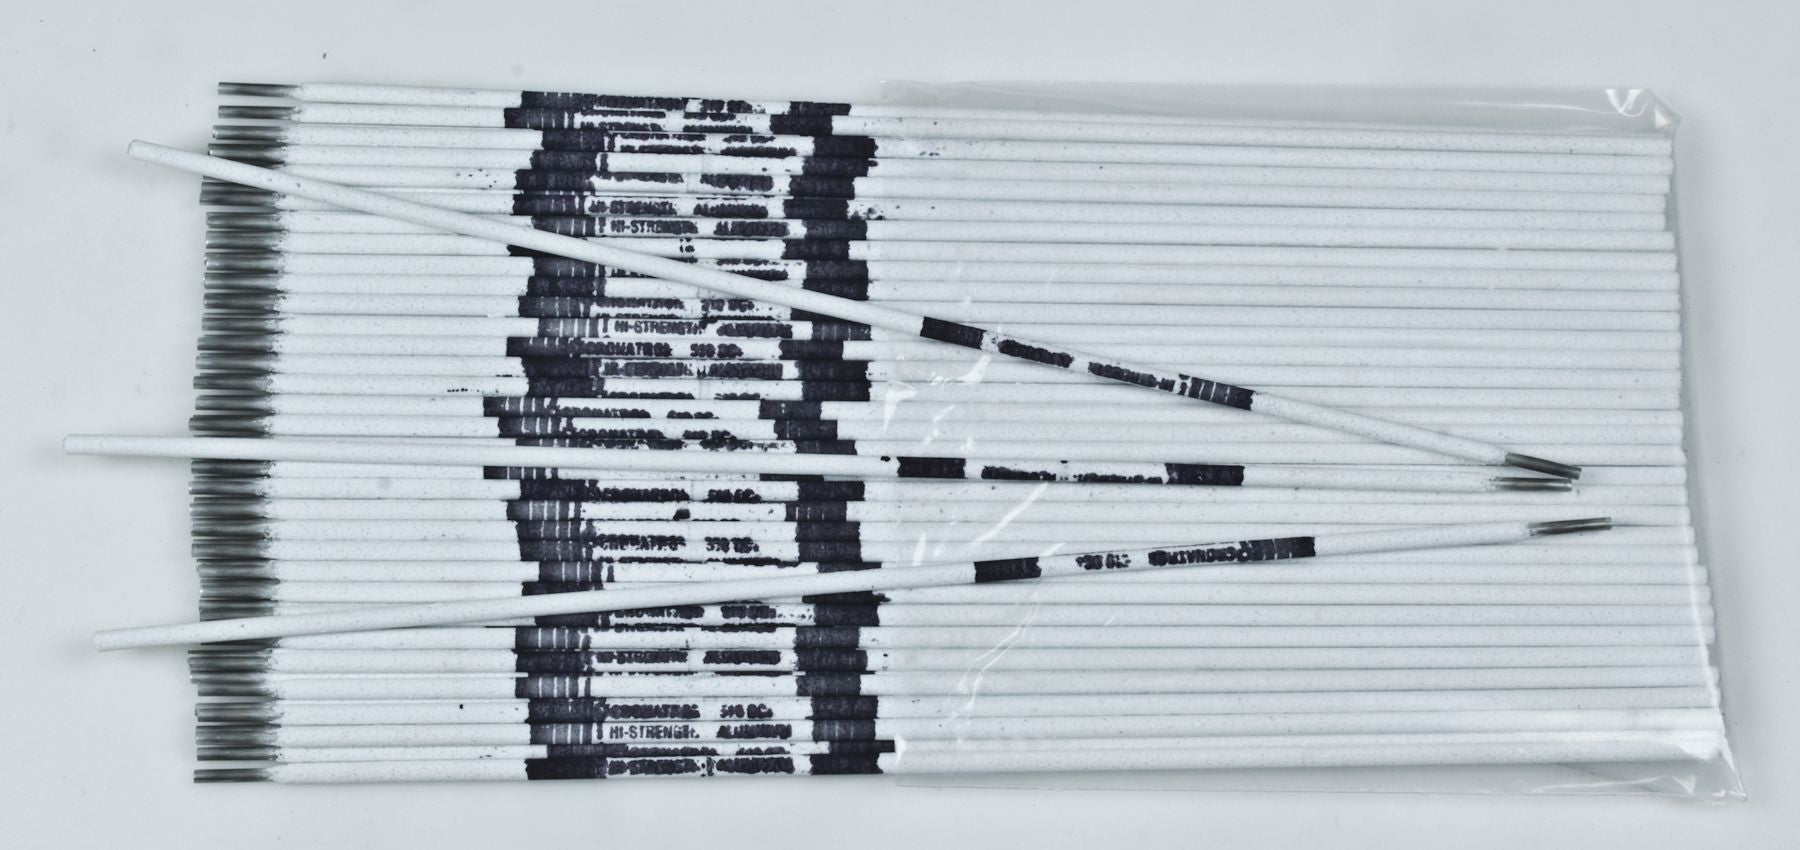
510 Aluminum Stick Rod Electrode 1/8"
Couldn't load pickup availability
333 Dissimilar Steel TIG Wire 3/32"
Couldn't load pickup availability
163 Arc-Cut Synthetic Carbon Arc Electrode
Couldn't load pickup availability
345 Tool Steel TIG Wire 3/32"
Couldn't load pickup availability
Product Description
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: DC Reverse
Usage ProcedureMaintain the shortest arc possible, using DC reverse polarity only. On large heavy sections, preheating to 400°F (204°C) will produce faster, flatter deposit with no splatter. Electrode should be held almost perpendicular and use a rapid stringer or weaving technique with a backwhip at the crater. Bevel pieces 75° on sections 1/8" (3.2mm) or thicker.
Technical Specifications
| Item#: | CW1826 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 3/32 " |
| Tensile Strength | 35,000 PSI |
| Base Metal | Aluminum |
| Polarity | DCRP |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 2.0 lb |