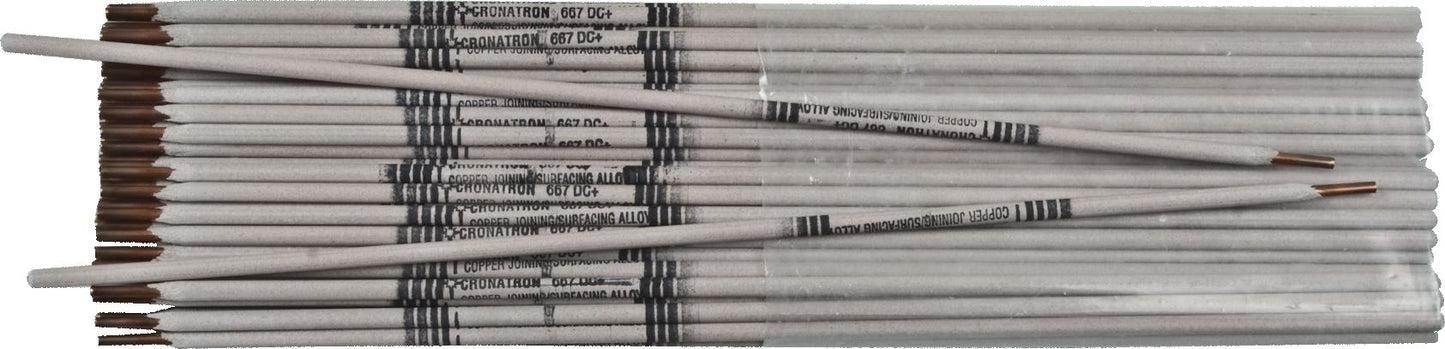
667 Copper and Brass Stick Rod Electrode, Flux Coated, 50-70 HRB Hardness, 100 to 130 Amps, 50% Elongation, DCRP Polarity, 1/8"
(Pack of
5)
SKU:CW1868 Item#: CW1868
An assortment of alloys for various copper, brass and bronze repairs.
Superior Advantages
• Corrosion-resistant
• Excellent color matches
• Highly versatile
Pure copper for high electrical conductivity
Tensile Strength: 35,000 PSI
Elongation: 50%
Hardness: Rb 50-70
Polarity: DC Reverse
Typical Applications
• Steel to copper repairs
• Galvanized steel
• Bronze valves and fittings
Usage Procedure
Use DC reverse polarity. A close arc should be maintained using a weave or stringer bead technique. Hold electrode perpendicular to workpiece. Preheating is unnecessary on light gauge material. Heavy sections should be preheated to 850°F to 1,000°F (454°C to 538°C). Slag can be removed easily with light chipping or brushing after cooling.
Frequently Bought Together
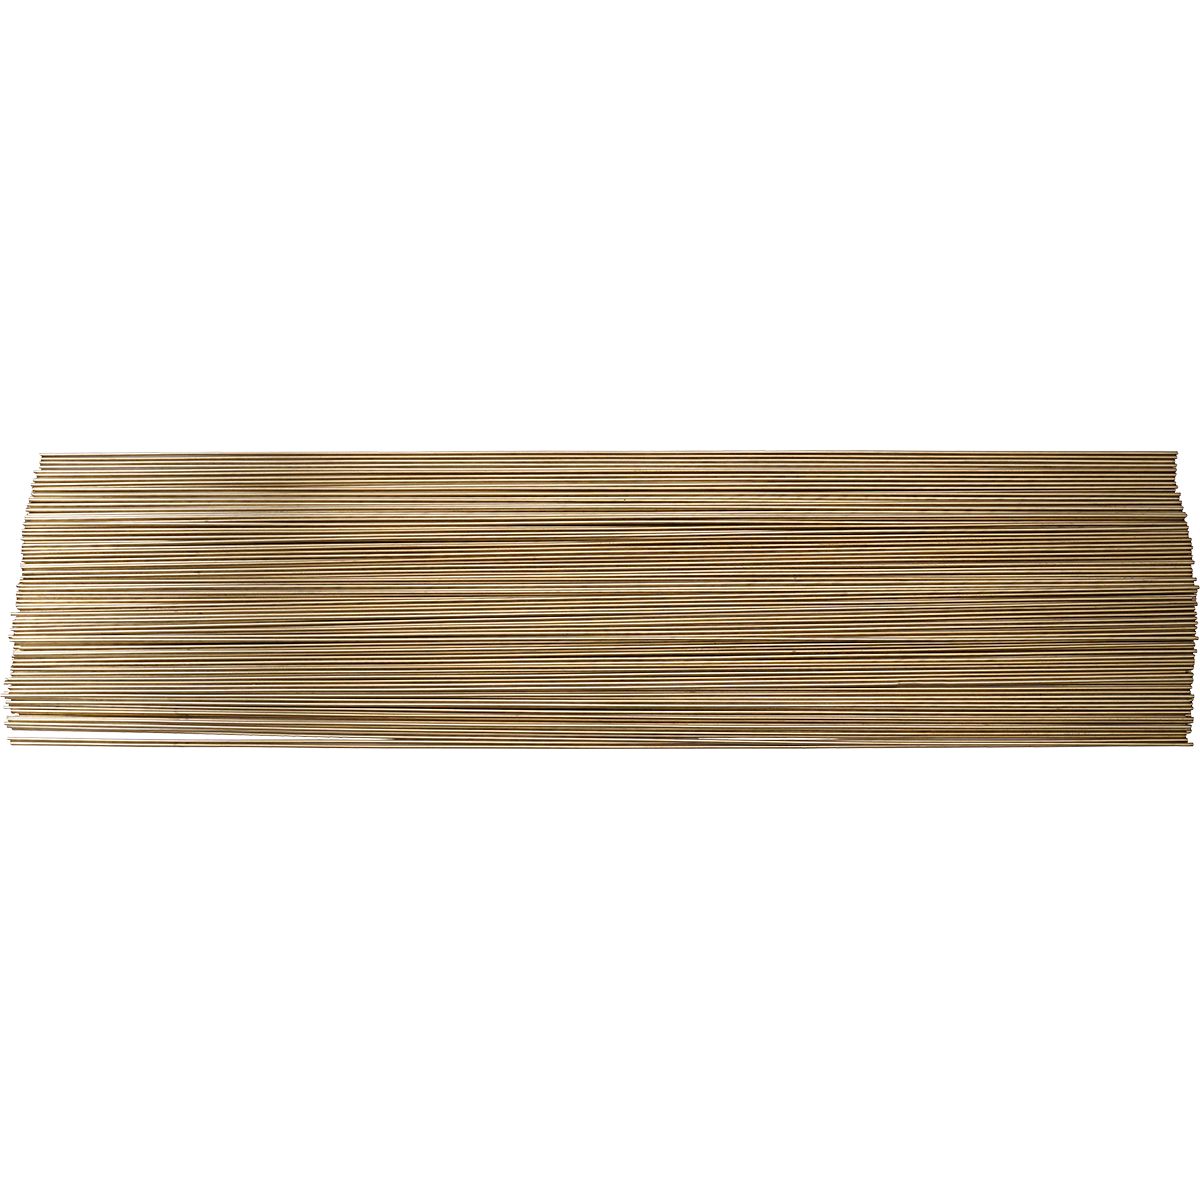
157T Premium Bronze Solid Tig Wire 1/16X36
Couldn't load pickup availability
Butt Connector 16 to 14 AWG Blue
Couldn't load pickup availability
Nylon Cable Tie 4" Black
Couldn't load pickup availability

180-degree Wide Beam Head Light with Side Light
Couldn't load pickup availability
Oxy Acetylene Fuel Gas Single Replacement Flint
Couldn't load pickup availability
Rosin Core Solder 1/16"
Couldn't load pickup availability
338 Mild/Carbon Steel Stick Rod Electrode 1/8"
Couldn't load pickup availability
333 Dissimilar Steel Stick Rod Electrode 1/8"
Couldn't load pickup availability
ER70S-6 Mild/Carbon Steel MIG Welding Wire 0.03"
Couldn't load pickup availability
E7018 Mild/Carbon Steel Stick Electrode 1/8"
Couldn't load pickup availability
Product Description
An assortment of alloys for various copper, brass and bronze repairs.Superior Advantages
• Corrosion-resistant
• Excellent color matches
• Highly versatile
Pure copper for high electrical conductivity
Tensile Strength: 35,000 PSI
Elongation: 50%
Hardness: Rb 50-70
Polarity: DC Reverse
Typical Applications
• Steel to copper repairs
• Galvanized steel
• Bronze valves and fittings
Usage Procedure
Use DC reverse polarity. A close arc should be maintained using a weave or stringer bead technique. Hold electrode perpendicular to workpiece. Preheating is unnecessary on light gauge material. Heavy sections should be preheated to 850°F to 1,000°F (454°C to 538°C). Slag can be removed easily with light chipping or brushing after cooling.
Technical Specifications
| Item#: | CW1868 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 1/8 " |
| Tensile Strength | 35,000 PSI |
| Elongation | 50 % |
| Base Metal | Copper/Brass |
| Hardness | 50-70 HRB |
| Polarity | DCRP |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 5.2 lb |
Product Restrictions