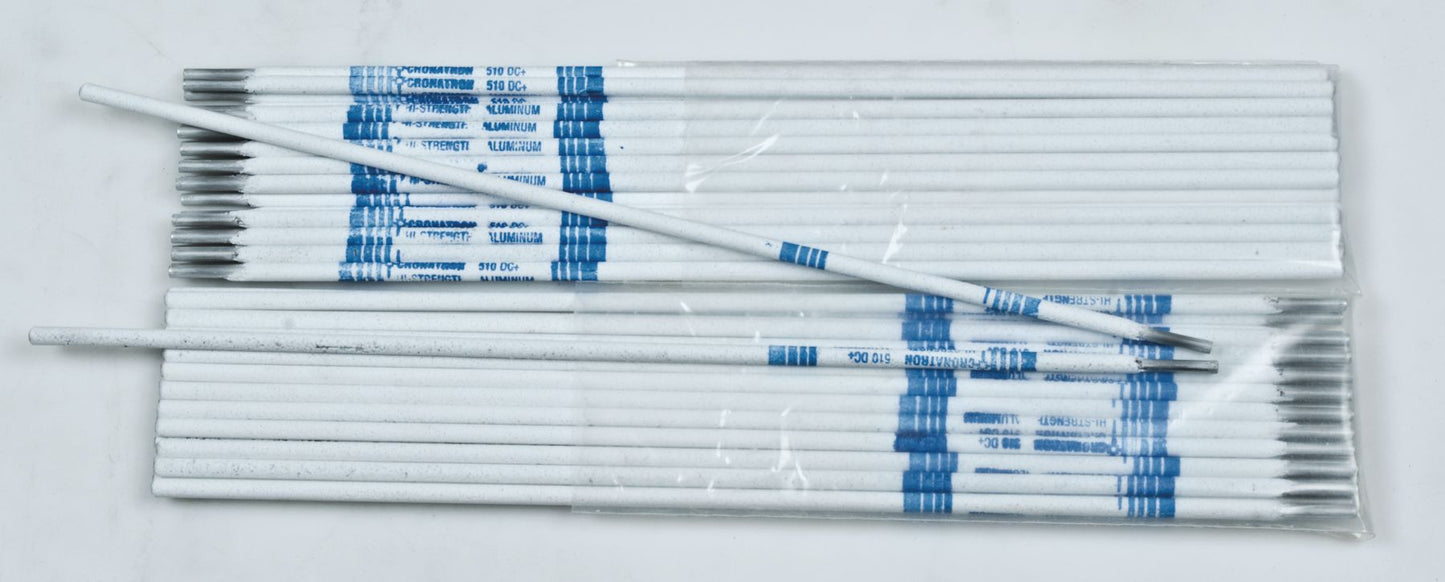
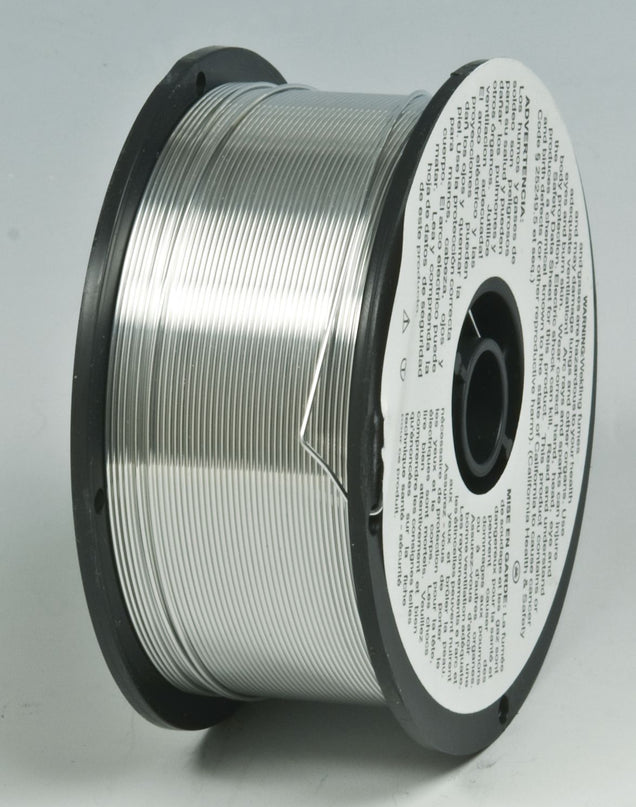
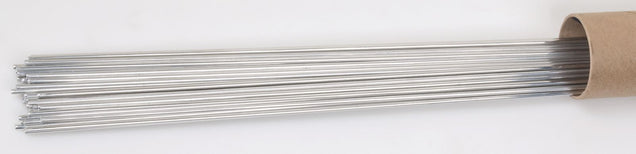
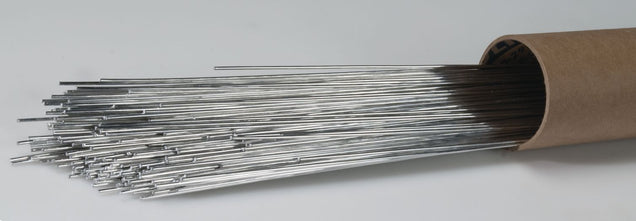
510 Aluminum Stick Rod Electrode, Flux Coated, 105 to 160 Amps, DCRP Polarity, Good Corrosion Resistance, Stable, Quiet Arc, 5/32"
(Pack of
2)
SKU:CW1038 Item#: CW1038
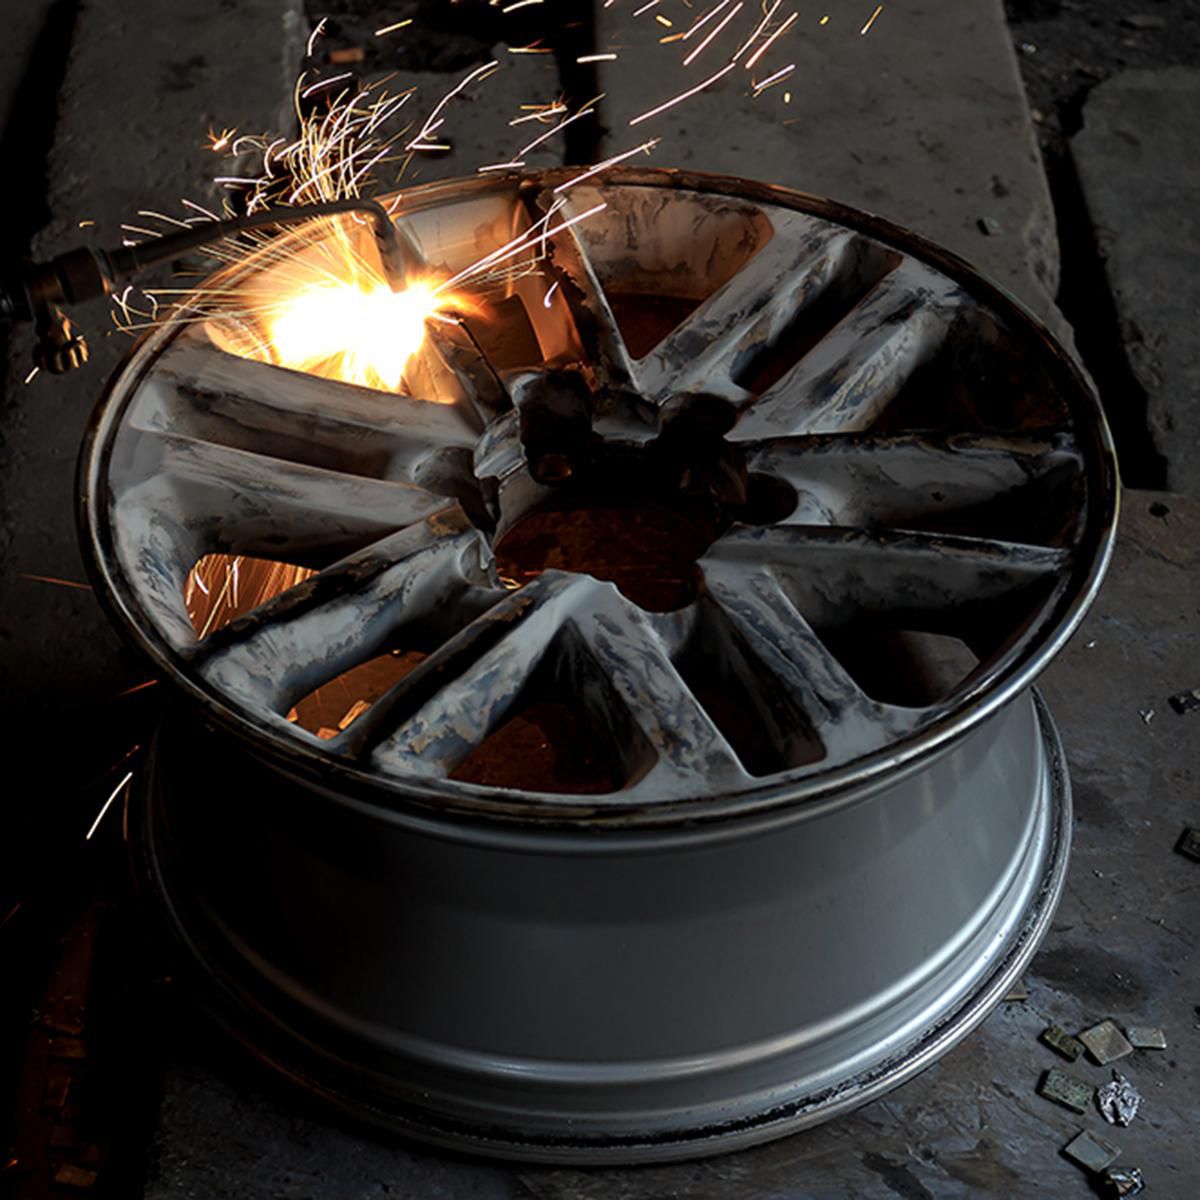
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.
Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: DC Reverse
Usage ProcedureMaintain the shortest arc possible, using DC reverse polarity only. On large heavy sections, preheating to 400°F (204°C) will produce faster, flatter deposit with no splatter. Electrode should be held almost perpendicular and use a rapid stringer or weaving technique with a backwhip at the crater. Bevel pieces 75° on sections 1/8" (3.2mm) or thicker.
Couldn't load pickup availability
Catalog page#: 13-16
Frequently Bought Together
ER4043 Aluminum MIG Welding Wire 0.035"
Couldn't load pickup availability
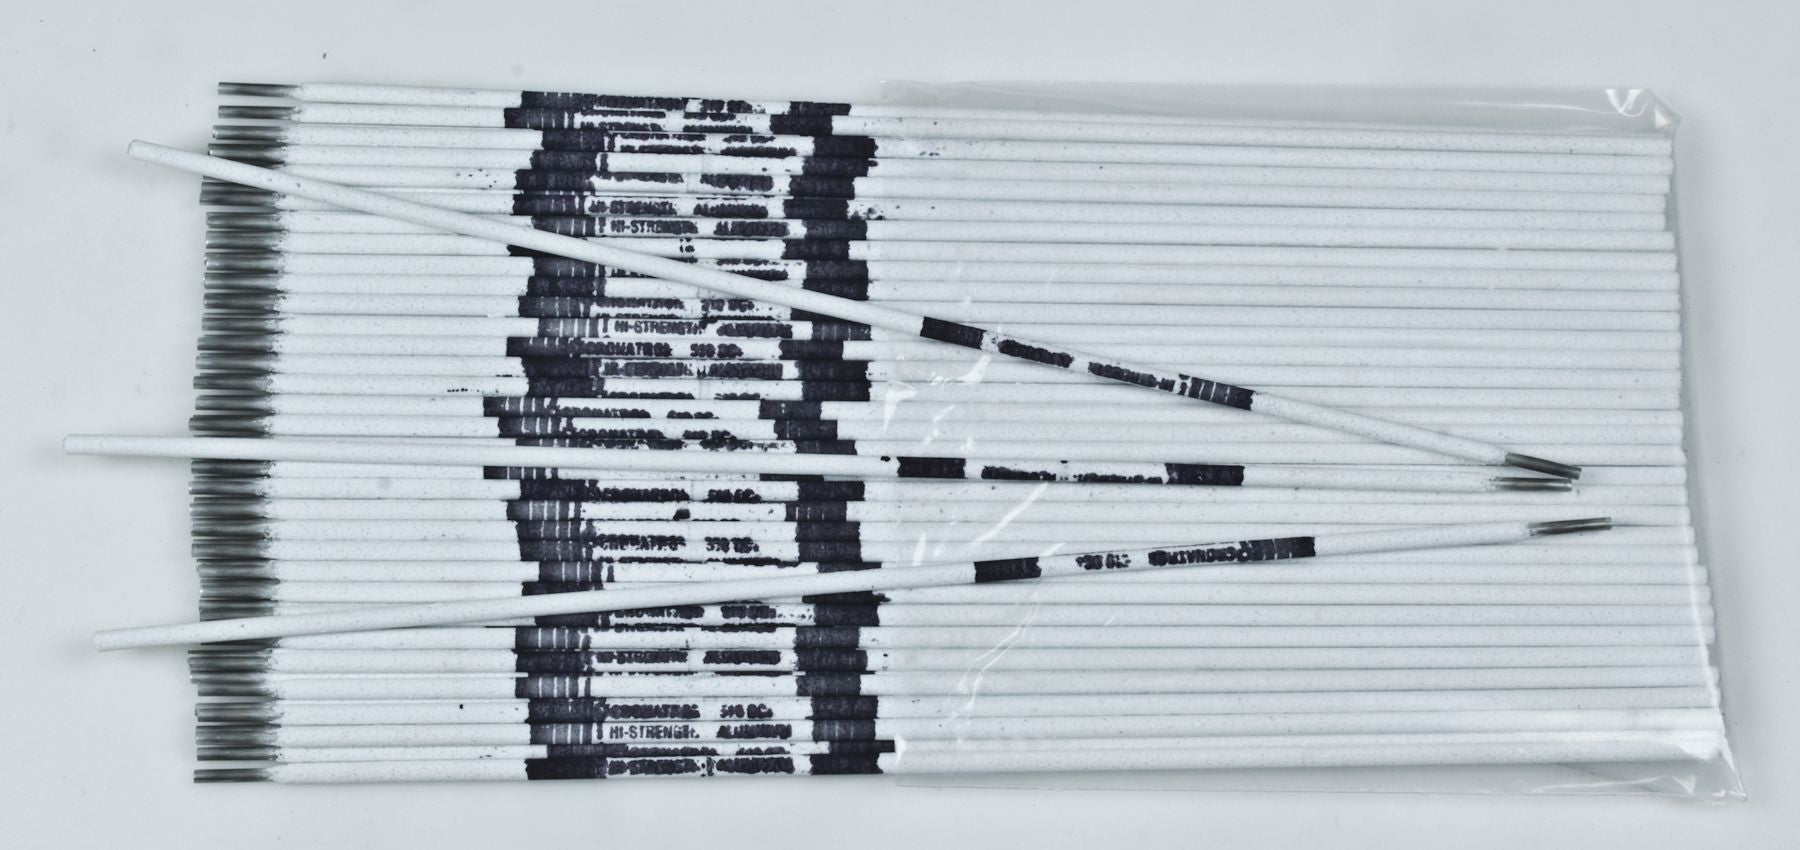
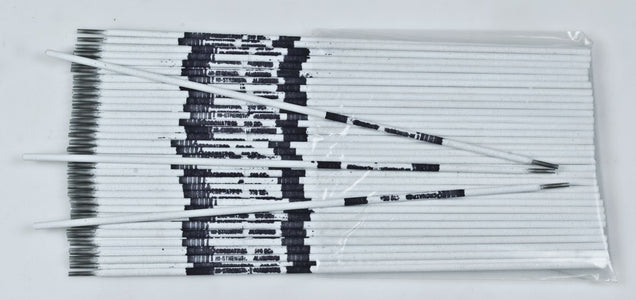
510 Aluminum Stick Rod Electrode 1/8"
Couldn't load pickup availability
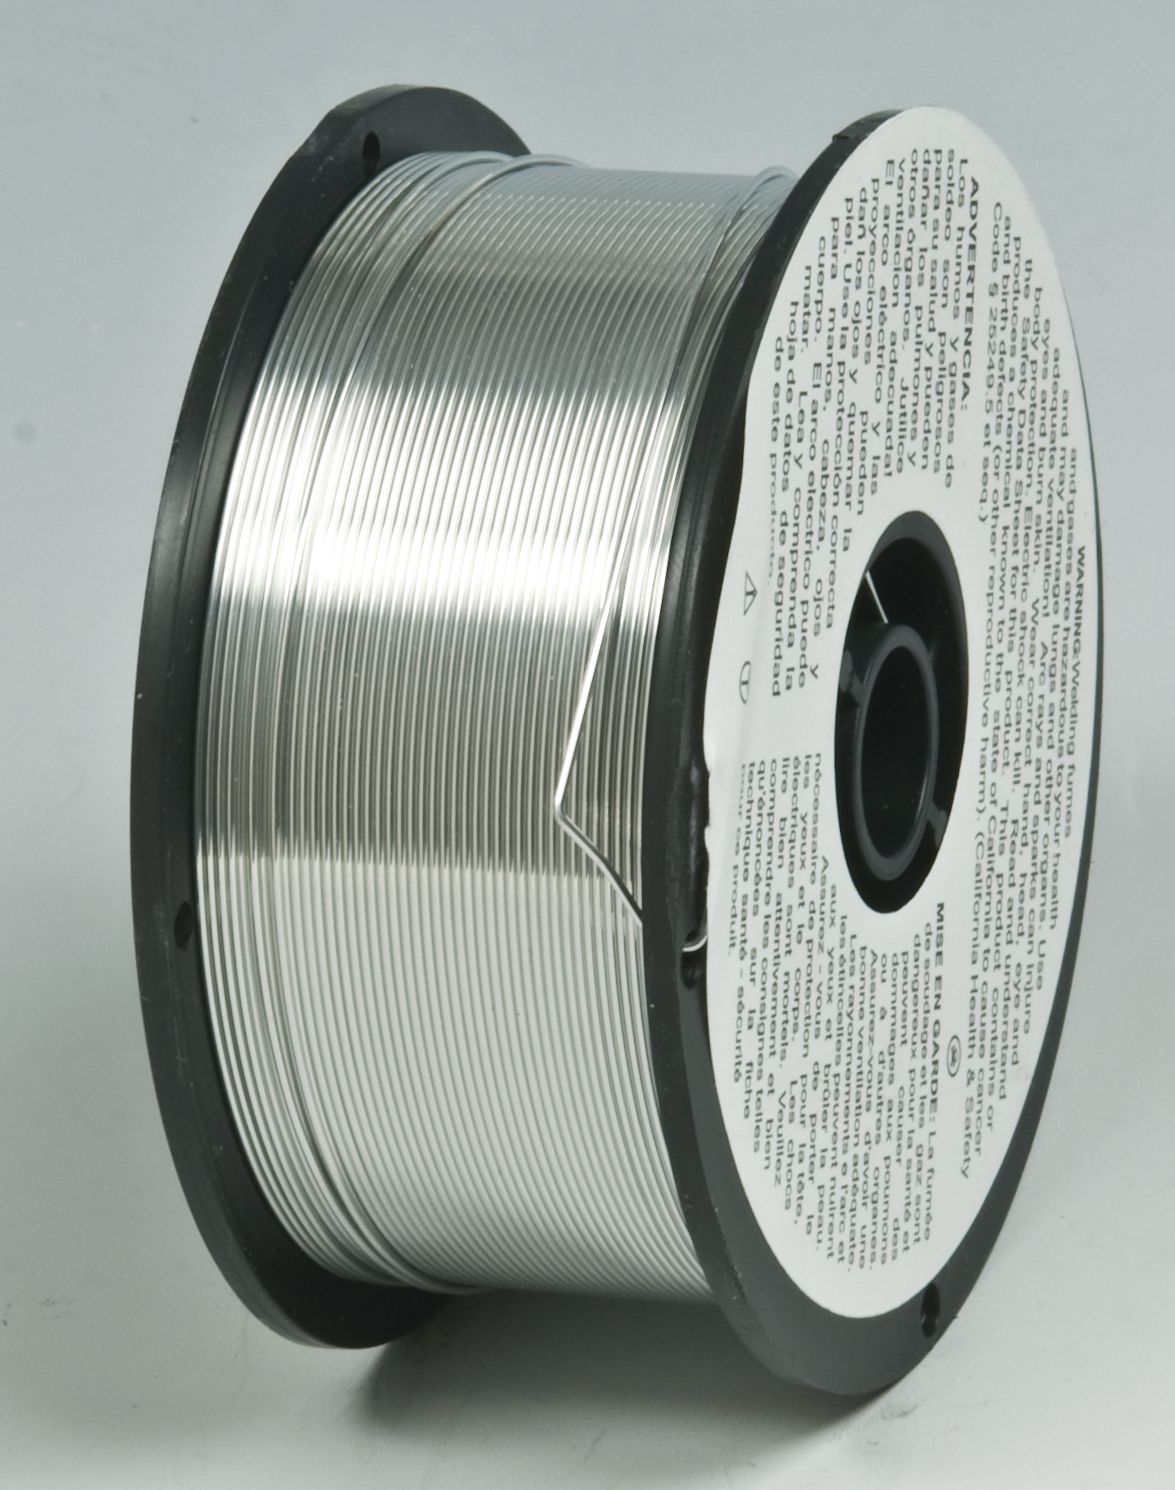
510 Aluminum MIG Welding Wire 0.035"
Couldn't load pickup availability
Superbutt Connector 16 to 14 AWG Blue
Couldn't load pickup availability
Self-Drilling Screw Hex Head #10-16 x 3/4"
Couldn't load pickup availability
Superbutt Connector 22 to 18 AWG Red
Couldn't load pickup availability
331 Mild and Carbon Steel MIG Welding Wire 0.03"
Couldn't load pickup availability
750 Martensitic Hard Facing Stick Electrode 1/8"
Couldn't load pickup availability
Carbon Air Arc Stick Rod Electrode 1/4"
Couldn't load pickup availability
211 Cast Iron TIG Wire 1/8"
Couldn't load pickup availability
163 Arc-Cut Synthetic Carbon Arc Electrode
Couldn't load pickup availability
345 Tool Steel TIG Wire 0.035"
Couldn't load pickup availability
Product Description
Highly versatile alloys for all weldable types of aluminum including sheet, forgings, extrusions and castings.Superior Advantages
• Stable, quiet arc with no undercutting
• Good corrosion resistance
Tensile Strength: 35,000 PSI
Polarity: DC Reverse
Usage ProcedureMaintain the shortest arc possible, using DC reverse polarity only. On large heavy sections, preheating to 400°F (204°C) will produce faster, flatter deposit with no splatter. Electrode should be held almost perpendicular and use a rapid stringer or weaving technique with a backwhip at the crater. Bevel pieces 75° on sections 1/8" (3.2mm) or thicker.
Technical Specifications
| Item#: | CW1038 |
|---|---|
| Welding Process | Stick |
| Type | Flux Coated |
| Diameter | 5/32 " |
| Tensile Strength | 35,000 PSI |
| Base Metal | Aluminum |
| Polarity | DCRP |
| UNSPSC #: | 23271810 |
| TAA Compliant: | Yes |
| Weight: | 2.0 lb |